Abstract
Fe-based shape memory alloys (Fe-SMAs) belong to smart metallic materials that can memorize or restore their preset shape after experiencing a substantial amount of deformation under heat, stress, or magnetic stimuli. Fe-SMAs have remarkable thermomechanical properties and have attracted significant interest because of their potential merits, such as cost-effective alloying elements, superior workability, weldability, a stable superelastic response, and low- temperature dependence of critical stress required for stress-induced martensitic transformation. Therefore, Fe-SMAs can be an intriguing and economical alternative to other SMAs. The recent advancements in fabrication methods of conventional metals and SMAs are helping the production of customized powder composition and then customized geometries by additive manufacturing (AM). The technology in these areas, i.e., fabrication techniques, experimental characterization, and theoretical formulations of Fe-SMAs for conventional and AM has been rapidly advancing and is lacking a comprehensive review. This paper provides a critical review of the recent developments in Fe-SMAs- related research. The conventional and AM-based methods of producing Fe-SMAs are discussed, and a detailed review of the current research trends on Fe-SMAs including 4-D printing of Fe-SMAs are comprehensively documented. The presented review provides a comprehensive review of experimental methods and processes used to determine the material characteristics and features of Fe-SMAs. In addition, the work provides a review of the reported computational modeling of Fe-SMAs to help design new Fe-SMA composition and geometry. Finally, different Fe- SMAs-based applications such as sensing and damping systems, tube coupling, and reinforced concrete are also discussed. This work will guide new research opportunities for working on Fe-SMAs and encourage new developments in the future.
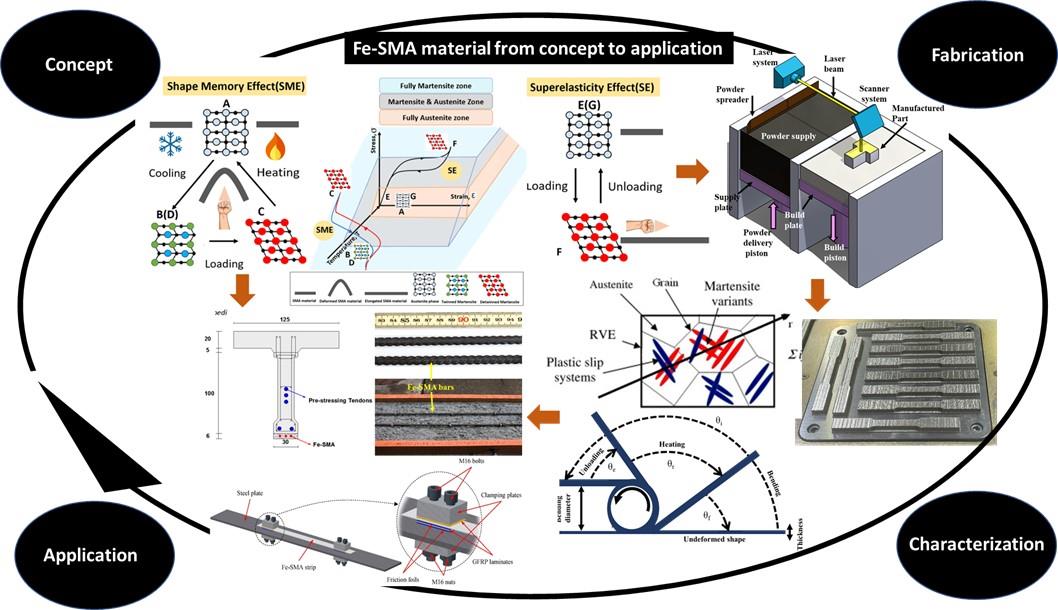
Graphical Abstract
Fe-based Shape Memory Alloy; Smart Materials; Additive Manufacturing; Functional Properties; Recent Advancements.
Abbreviations
Af, austenite finish temperature; As, austenite start temperature; AM, additive manufacturing; ANN, artificial neural network; BCC, body-centered cubic; BCT, body-centered tetragonal; CAD, computer-aided design; DMA, dynamic mechanical analyzer; DSC, differential scanning calorimeter; ECCI, channeling contrast imaging; EBSD, electron backscatter diffraction; FCC, face-centered cubic; HCP, hexagonal- close-packed; HTSMA, high-temperature shape memory alloy; ICP, inductively coupled plasma; LPBF, laser powder bed fusion; MA, mechanical alloying; Mf, martensitic finish temperature; Ms, martensitic start temperature; MTs, martensitic transformations; OM, optical microscopy; OWSME, one-way shape memory effect; PE or SE, pseudo-elasticity or superelasticity; SEM, scanning electron microscopy; SMAs, shape-memory alloys; SME, shape memory effect; SMMs, shape-memory materials; SR, strain recovery; TEM, transmission electron microscopy; TH, thermal hysteresis; TTs, transformation temperatures; TWSME, two-way shape memory effect; VAR, vacuum arc melting; VED, volumetric energy density; VIM, vacuum induction melting; XRD, X-ray diffraction.
Ntroduction
Smart materials are defined as those that can perceive their environment and/or own states, make a judgment, and then modify their functions following a predetermined purpose . Their smart behavior includes a change in the geometry size, shape, or color in reaction to a variety of externally performed stimuli including light, stress, temperature, pH, moisture, and electric or magnetic fields , ., . Shape memory materials (SMMs) are smart materials that can restore their predefined shape after experiencing considerable deformation with exposure to a particular stimulus, such as heat, stress, or magnetic induction . Numerous materials, including ceramics, polymers, metals, and composite materials, exhibit the shape memory phenomenon , , , , .
Shape memory alloys (SMAs) are one common category of SMMs that have excellent thermomechanical characteristics and can restore their undeformed shape after being subjected to a certain temperature or load , . SMAs have been employed in various industrial and medical fields since their discovery in 1932, including robotics, biomedical, aerospace, and mechanical engineering . Crystallographic phases are what enable SMA performance in which reversible transformations from one material phase to another take place via diffusion-less transformations known as reversible martensitic transformations (MTs). This phase change is related to the distinct properties including pseudo-elasticity (PE) or superelasticity (SE) and shape memory effect (SME) that set SMAs apart from other materials. Temperature-induced reversible transformations result in SME, whereas stress-induced transformations lead to PE , , , , , .
The shape memory performance was first investigated in Au-Cd alloys. After that, several SMAs including Ti-Ni, Ni- Co-Mn-In, Ni-Mn-Ga, and Cu-Al-Ni have been described. Due to PE, SMAs such as Cu-Zn-Al and Ni-Ti display a significant recoverable strain. The Ni-Ti–based alloy, particularly, is the only superelastic material currently produced due to its ductility and outstanding superelastic strain , . SMAs are known for a variety of distinctive phenomena, including SME, SE, enormous damping capacity, and a two-way SME . SMAs have high conductivity so electrical current can be employed for their electrical resistive heating .
Ni-Ti SMA has received interest since its discovery in 1959 due to its outstanding SE, high recovery strain, and corrosion resistance. Nevertheless, the high cost and time-consuming processing combined with the need to produce NiTi SMA with suitable properties minimize its applications on a broad scale , . Despite all efforts exerted on NiTi SMA investigation, no viable binary NiTi SMA with a transition temperature greater than 150 °C has been discovered , . In general, NiTi SMAs are still too costly for a variety of applications and there is a need to explore alternate options that have higher transition temperatures, are more stable, and have appropriate strength and ductility.
Iron-based SMAs or Fe-SMAs have outstanding characteristics including superior workability and weldability, low- temperature dependency of transformation critical stress, and stable superelastic behavior over a wide temperature range , , , , . Fe-SMAs can exhibit lower thermal hysteresis and nearly identical martensitic phase transformation behavior to that of nitinol SMA such as Fe–Ni–Co, Fe–Pd, and Fe–Pt alloys. However, Fe–Pd or Fe– Pt Fe-based alloys do not typically display PE at ambient temperature. Fe-SMA with higher thermal hysteresis including Fe–Mn–Si and Fe–Ni–C can demonstrate significant SMEs , , , , .
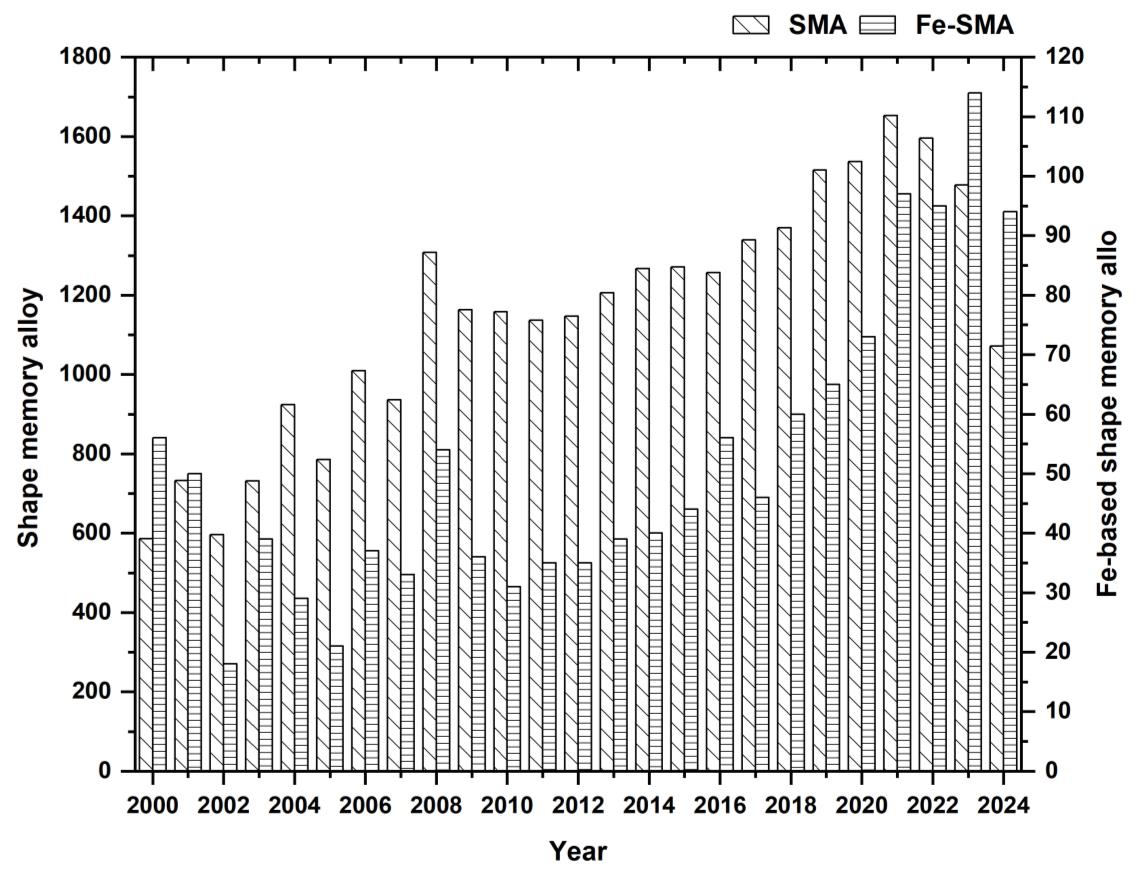
Additive Manufacturing (AM) technologies advance metals and SMAs fabrication, enabling the processing of customized powder composition and customized geometries. However, a comprehensive review of the fabrication techniques, experimental characterization, and theoretical formulations of Fe-SMAs is still lacking. This work aims to fill this gap by providing an in-depth review of the development, properties, mechanisms, and classification of Fe- SMAs. The work examines the experimental methods and processes used to ascertain the essential characteristics and features of Fe-SMAs. Theoretical research on Fe-SMAs has been addressed to enable the development of models that various methods proposed for modifying Fe-SMAs and enhancing their performance—including alloying elements, the materials' textures, and structures, as well as the deformation temperature, grain (abnormal growth, size, orientation, and morphology), and using heat treatment techniques. The article highlights the most recent research on the Fe-SMAs and their future directions including AM-produced Fe-SMAs. Fe-SMAs-based applications such as reinforced concrete, tube coupling, and sensing and damping systems are comprehensively reviewed. Fig.1 illustrates the publication's survey of Fe-SMAs and other SMAs. The number of publications in 2000-2024 through Web of Science accessed on September 20, 2024, where the number of publications on Fe-SMAs is growing.
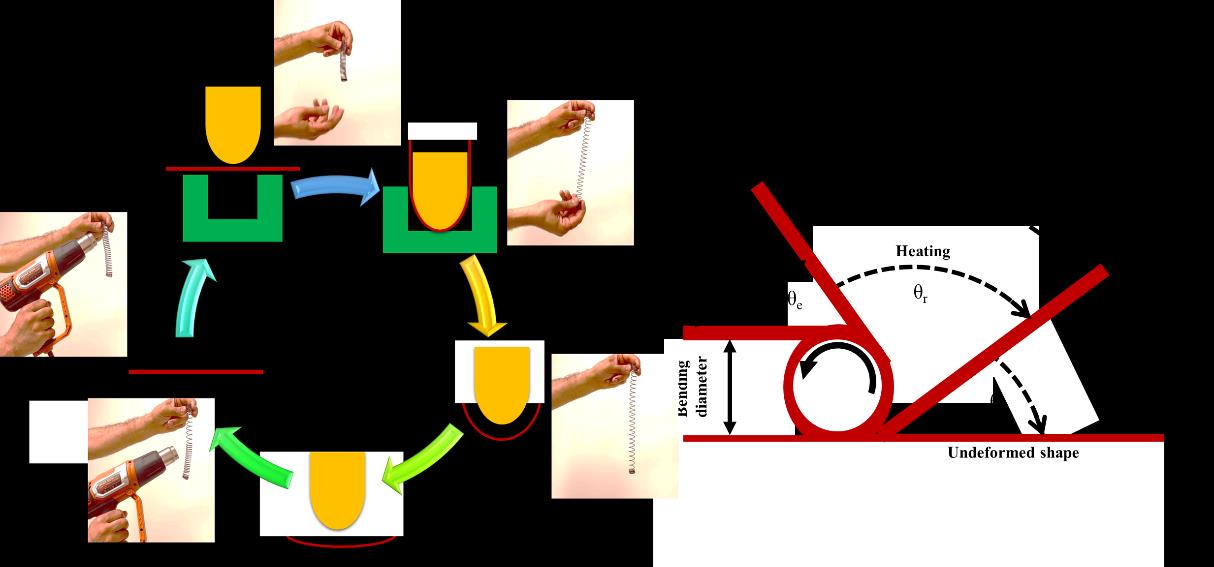
Fig. 1. Publications survey of Fe-SMAs and other SMAs. The number of publications in 2000-2024 through Web of Science accessed on September 20, 2024. 2. Evolution, Classification, and Mechanisms of Fe-SMAs 2.1. Ni- and Cu-based SMAs.
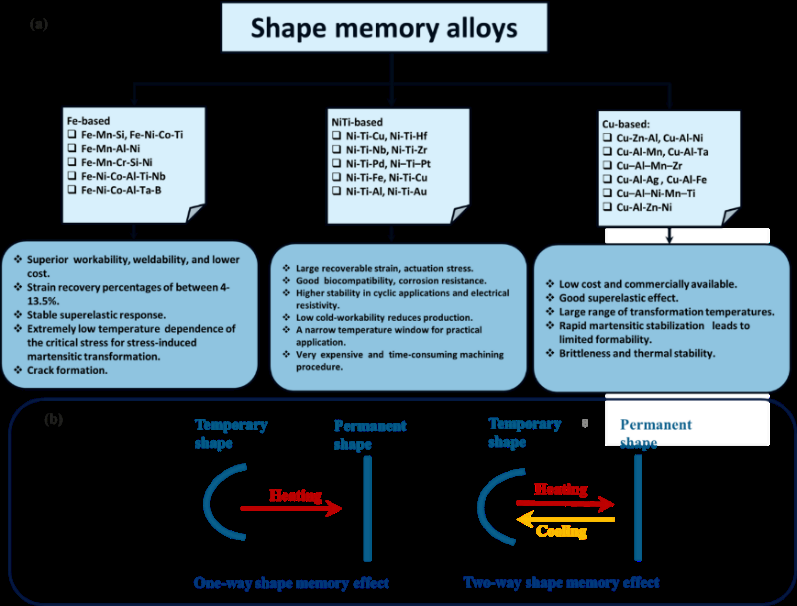
The SMAs are classified into copper-based, nickel-titanium-based, and iron-based SMAs as illustrated in Fig.2a. The NiTi-based SMAs are robust on several levels, namely large reversible strain, good actuation stress, and corrosion resistance. They are produced mostly using Ti and Ni elements and other alloying elements such as Hf, Ti, Cu, Fe, and Zr , , , . They have notable features such as SE and SME, as well as better functional fatigue and biocompatibility. However, they are still considered expensive and difficult to process and produce with designed optimal features. In addition, they are quickly fractured when subjected to substantial deformations of more than 30% compared to those developed under intermediate annealing or cold rolling processing. They also exhibit insufficient ductility for practical applications and their maximal martensitic start temperature (Ms) of NiTi-SMAs cannot surpass 360K , . The reduced production and increased manufacturing costs of NiTi SMAs due to their high sensitivity to compositional changes in their transformation temperatures (TTs), difficulties in cold forming due to their ordered intermetallic structure, and complexity in joining such materials, have slowed their commercialization and restricted their applicability to a broad range of industries , , , , , .
Fe-based and Cu-based SMAs, such as Fe-Mn-Si and Cu-Al-Ni, are other types of SMAs. They are characterized by their low costs, commercial availability, good workability/weldability, as well as large temperature range for SE , , . They are also classified as alloys with high transformation temperatures (HTSMA) as their reverse transition begins only at temperatures above 120 °C (390 K) in a stress-free state , . The wide range of TTs and flexibility of iron and copper-based SMAs allow for customizing the composition, processing, and optimizing their properties . The common challenges in Cu-based SMAs include brittleness and thermal stability because of large grain sizes and γ1 (Cu9Al4) separation, especially in polycrystalline alloys. Several factors typically enabled the production of components with better strength and ductility such as the development of copper-based single-crystal SMAs, which can provide notable SE, and using AM methods to create complicated shape Cu-based SMAs with rapid cooling rates , .
SMAs can also be classified according to the type of SME, as illustrated in Fig.2b. The first type is the one-way SME (OWSME) with austenite arrangement recovered. This OWSME type is present in the majority of commonly used SMAs and is defined by the process of recovering the undeformed shape after heating the deformed specimen to a temperature higher than the finishing temperature of austenite. On the other hand, a two-way SME (TWSME) is defined when austenite shape recovers at high temperatures and martensite arrangement returns at low temperatures.
Alloys with TWSME are less commonly utilized commercially because of the extra training demand. The TWSME generally yields less reversible strain compared to OWSME for the same alloy , , . Furthermore, its strain quickly deteriorates, particularly at high temperatures . Typically, OWSMA offers a more reliable and cost-effective solution. The TWSME was generated in Ni-29.7Ti-20Hf alloy using repeated thermal cycling over its martensitic transition under shear stress . The TWSME was also apparent in the Ni-24.28Al-18.53Fe alloy with two phases of microstructure. The TWSME of martensite and γ -phase samples quenched from 11850 °C was as high as 34 % at a strain of 0.33 %, but the TWSME of γ-β phases specimens quenched from 1100 °C was only 8.8 % at a strain of 0.66 percent, rising to 22.5 % when the strain was increased to 1.38 % . This indicates that the TWSME varies significantly with the phase composition and the quenching temperature, as well as the applied strain.
Evolution Of Fe-Smas
Fe-Mn-Si alloy is the first iron-based alloy with the SME to be reported in 1982 by Sato et al . Since then, Fe- SMAs including Fe-Ni-C , Fe-Mn-Si , , Fe-Ni-Co-Ti , , , and Fe-Mn-Al have gained significant interest due to their superior weldability, workability, and cheaper processing than the commonly produced NiTi SMAs. Those Fe-SMAs have a limitation in achieving SE at ambient temperature due to their MTs between different phases (γ to ε [face-centered cubic (fcc) / hexagonal- close-packed (hcp)] and γ to α′ [ body-centered cubic (bcc) / body-centered tetragonal (bct)] are generally none thermoelastic. Although the thermoelastic transition (fcc/face-centered tetragonal (fct)) of Fe-Pd and Fe-Pt alloys are well-known, no SE at ambient temperature has been reported since 1984 . To enhance the performance of Fe-SMAs, extensive research has been carried out.
These studies showed that the alloying additives had a significant impact on the SME of these alloys. Forming NbC precipitates in Fe–Mn–Si SMAs achieved higher SME , . Precipitation and composition modifications were effective in inducing thermoelastic transformations with lower thermal hysteresis in certain Fe-SMAs . Their recovered strains, on the other hand, were less than 3%, limiting their use to exceptional applications like big-diameter pipe couplings , . The inclusion of VC in Fe-SMAs resulted in attractive and promising features for applications of reinforcement and concrete structures. VC-based Fe-SMAs showed good properties with no training after manufacturing them under conventional air melting and casting circumstances , , , , .
Fe-SMAs can be used in a variety of sectors that demand vast amounts of materials, such as building or construction. The main shortcomings of Fe-SMAs are their non-thermoelastic transformation, which results in extremely high- temperature hysteresis (i.e., greater than 300 °C) and a lack of SE . Although Fe-SMAs have long been known, the development of FeNiCoAlTaB and FeMnAlNi alloys marked a turning point in Fe-based SMA design. In their polycrystalline state, FeNiCoAlTaB alloys are reported to exhibit significantly higher levels of a superelastic strain than nickel-titanium alloys. These Fe-SMAs have a high superelastic strain and are significantly stronger, as a result, they have a better capacity for absorbing energy compared to Cu and NiTi SMAs. They produced a superelastic strain higher than 13% and an ultimate strength of more than 1 GPa, which is nearly double that obtained by Ni-Ti alloys . These Fe-SMAs can be used in strain sensing and energy-damping applications due to their outstanding properties. To induce such properties, the system must be precipitate hardened, cold rolled to impart the orientation, and embedded with the Boron element for grain refinement . Fe-Mn-Al-Ni SMAs have a minor temperature dependency of the critical stress due to a low transformation entropy shift generated by the Gibbs energy effect. Across a temperature range of –196 to 240 °C, the superelastic stress for Fe-Mn-Al-Ni SMA was varying by 0.53 MPa/°C . Later investigations were conducted on single-crystalline FeNiCoAlTa alloy and elaborated on the MTs and the orientation dependency of SE. Under tensile testing, FeNiCoAlTa SMAs showed a strain recovery of 6.8%, 130 MPa of stress hysteresis, and a wide temperature range of 130 °C in a single crystalline state of orientation. On the other hand, high-stress hysteresis values of 350-400 MPa, low superelastic strain values of 2.0 %, and a superelastic temperature range of 55 °C were obtained in single crystals with orientation , . The shape memory characteristics were tested for FeNiCoAlNb SMA in single crystal form along orientation using SE tests in tension and compression conditions. The highest SE of around 11.5% was obtained in compression testing.
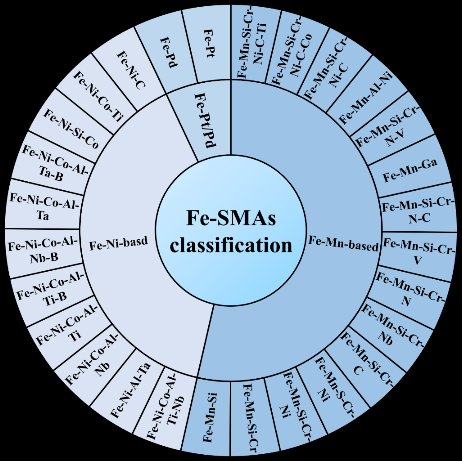
The results demonstrated that SE significantly relies on stress conditions . The aging of the alloy resulted in γ′- and β-phase precipitates. The induced SE was investigated between the starting martensite temperature (Ms) and the austenite finishing temperature (Af), as well as between Af and 323–373 K . The transformation temperatures of FeNiCoAlTiNb SMA were confirmed using thermo-magnetization under superconducting quantum interference at 0.05 and 7 Tesla . The summary of the development and classification of Fe-SMAs is shown in Fig.3 and Table 1.
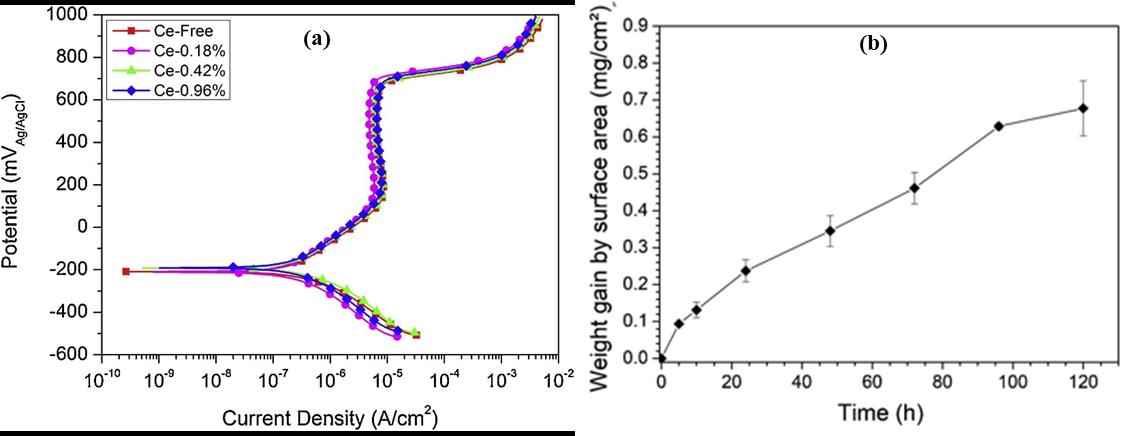
Fig. 2. Classification and comparison of SMAs. (a) Classifications, advantages, and disadvantages of shape memory alloys and (b) A schematic of one-way SME and two-way SME behaviors of shape memory alloys. 3. Classification of Fe-SMAs showing the concentration of research on Fe-Mn/Fe-Ni based SMAs.
Echanisms Of Fe-Smas
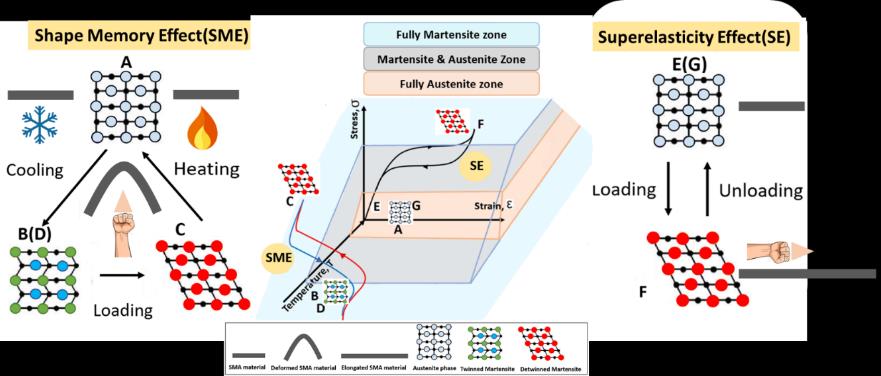
SE and SME are the distinctive functional properties that distinguish SMAs from other materials and allow for their usage in a variety of industrial applications , . These metallic alloys' remarkable characteristics are due to the MT that is induced under either temperature or stress , , . The contributing factors to this transformation are the austenite and martensite phases of SMAs. The austenite phase has a symmetric crystalline structure and is often stable at elevated temperatures and moderate stresses. The martensite phase, on the other hand, has a lattice structure with minimal symmetry and is usually stable under high stresses and low temperatures , . The phase change occurs among them by rearranging the positions of particles within the solid's crystal structure as shown in Fig.4. Overall, beginning with the twinned martensite,(point D) in Fig.4, that is created after cooling the austenite phase (point G), external loading causes the twinned martensitic microstructure to deform due to the lattice's reorientation and detwinning resulting in so-called detwinned martensite (point F) as illustrated in Fig. 4. The ability of SMA material to accommodate strain in such a way as to produce a twinned martensite structure (point B) is its unique property. As the martensitic structure (detwinned, point C) experiences subsequent thermal flow (heating), the low-symmetry martensitic microstructure then undergoes a second transformation into the well-ordered, more stable, and high-symmetry austenite structure (point A). This microscopic distortion is the key to the recovery of the material's original shape , , , . In the SE effect (Point G to F), external stress causes the material to transform from the high-symmetry, elevated-temperature, well-ordered austenite phase to the lower-symmetry martensite phase.
This change takes place in a temperature interval where the martensitic phase is unstable without loading; hence, upon unloading, the phase reverts to the original austenitic form, reversing the deformation. Numerous iron alloys have been the subject of SE research, and various strategies have been developed to improve them , , , , , . It can be concluded that the ability to reverse the austenite/ martensite interface is the most significant requirement for inducing the unique features of the Fe-SMA system.
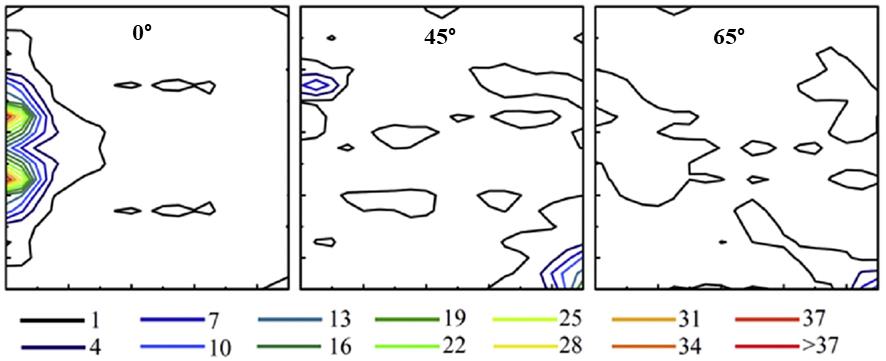
Table 1. Historical growth of Fe-SMAs with their specific compositions over the last decades
, , ,
The transformation can occur from fcc to hcp, as in the FeMnSi alloy, or from bcc to bct, as in the FeNiCoTi and FeNiCoAlX alloys , , . The stress-induced transition of austenite to martensite (fcc to hcp) and its reversal (hcp to fcc) through heating is the basis of shape memory features in Fe-SMAs. The migration of Shockley partial dislocations via non-adjacent close-packed planes is investigated to be responsible for the creation of the martensite from the austenite , . The typical phase transformation of Fe-SMAs in the stress-free state is fully described using four different temperatures. The starting (Ms) and finishing temperatures (Mf) of forward MT, as well as the starting (As) and finishing temperatures (Af) of backward transformation. The martensitic forward transformation can be reversed by heating the material while it is in the martensitic region (T < Mf). The following is how the temperatures are organized: Mf < Ms < As < Af. There are no phase shifts when the temperature is changed at the range (Ms < T < As), and both phases can exist at (Ms < T < As) , , , . The shape memory characteristics can be fully represented using these four transition temperatures and the principle of self- accommodation. The MTs typically have thermal hysteresis (TH), which indicates that the forward and backward transformations do not proceed at the same temperature. TH in Fe-SMAs is often described as the difference between interfacial motion, during martensitic transformation. Large TH can produce substantial and steady recovery stresses, making Fe-SMAs with these characteristics, like Fe-Mn-Si SMAs, more suitable for structural applications .
Small TH, on the other hand, is favorable in other different applications, hence numerous experiments have been conducted to manufacture SMAs with thermal hysteresis of near-zero or as little as 0.4 °C , , , , , , . Copper doping of Fe-Ni-Co-Ti SMA showed a significant decrease of the TH width to ΔT ≈ 60 K, maintaining the Curie temperature at about 300 °C .
Fig. 4. Diagram showing the entire cycle Fe-SMA mechanism. The phase transformation of austenite(γ) to martensite (ε) and its reversal is illustrated with a microscopic demonstration of SE and SME. 3. Production, characterization, testing, and modeling of Fe-SMAs
Production Routes Of Fe-Smas
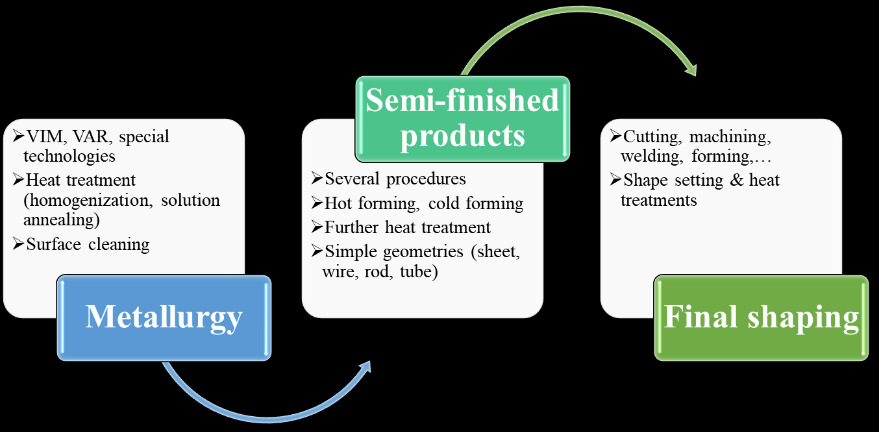
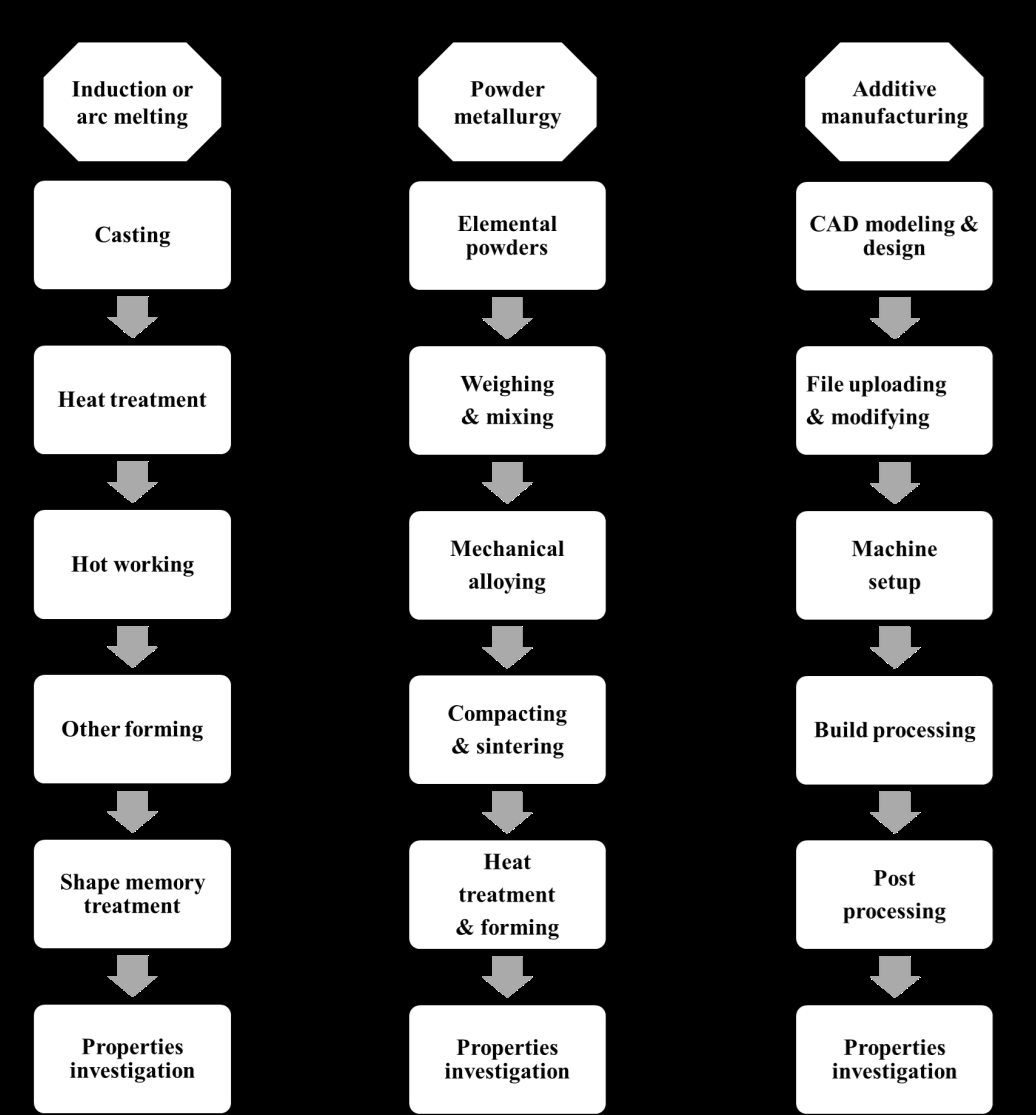
Fe-SMAs are produced as semi-finished items, such as rods, wires, ribbons, and tubes, or as finished products, such by several specialized companies all around the world , , , , , , . Melting and casting (Fig.6 (a)) are often the first steps in the preparation of most Fe-SMAs. Casting is commonly applied using either vacuum arc melting (VAR) or induction melting (VIM). These are specialized processes used to ensure that the metals are evenly mixed, and impurities are minimized in the alloy. Other subsequent procedures such as heat treatment, hot rolling, and drawing are followed to produce parts with variable shapes and minimal defects. Heat treatment is mainly applied for the homogenization process, followed by hot working and further treatments to enhance the mechanical and thermomechanical properties of the Fe-SMAs , , . After the preparation and treatment of the Fe-SMAs samples, thermomechanical, and other required properties can be determined. A summary of the different steps involved in Fe-SMAs conventional production is shown in Fig. 5.
Fig. 5. Conventional production procedures of Fe-based SMAs. Fe-17Mn-5Si-10Cr-4Ni SMA containing VC was fabricated using standard air-casting facilities followed by other heat treatments and characterizations to evaluate its properties . Fe-17Mn-5Si-5Cr-4Ni-1Ti-0.3C SMA was produced using casting, followed by forging and hot-rolling to produce SMA with the intended shape . A good summary of Fe-SMAs manufactured using conventional and modern methods is illustrated in Fig. 6 and a description of the fabrication processes used to synthesize Fe-SMA is listed in Table 1.
Alternatively, mechanical alloying (MA) has been used to produce Fe-SMA, Fig. 6(b) illustrates the steps of MA that involve solid-state reactions between powder particles brought on by high-energy interactions. MA is considered a powder metallurgy technology that has several benefits for the manufacture of Fe-SMA products, due to its ability to manufacture the components in almost net shape. This reduces the supplementary machining needed to shape the eventual product. The thermo-mechanical and mechanical properties of Fe-SMA produced by MA could be equivalent to that of conventional casting , . On the other hand, the use of conventional methods in Fe-SMA production has some limitations. Even though the VIM method can achieve good chemical homogeneity using electromagnetic stirring, the presence of titanium in the processed alloy can react with the graphite crucibles which results in TiC formation. These particles will modify the alloy composition and, consequently, the TTs , , . Chemical homogeneity of the ingots in the VAM technique needs multiple remelting processes due to insufficient stirring. The alloy absorbs oxygen and carbon during these remelting processes, which again has an impact on the TTs .
Complex structure fabrication using conventional techniques is time-consuming and so challenging. During manufacturing, excessive tool wear might be produced. In addition, it will be extremely difficult to create polycrystalline structures if the alloy is even slightly brittle , .
These issues and others can be overcome by using additive manufacturing (AM) techniques which eliminate the necessity for tooling and enable the manufacturing of SMA components of intricate geometries directly from CAD models. The manufacturing of Fe-SMAs has been improved with the new advancements in AM to create SMAs with improved characteristics , , , , . Fig. 6(c) lists the steps followed to fabricate Fe-SMA using AM. AM technologies represent considerable potential for improving the manufacturing of Fe-SMAs. They have been recently used for several Fe-SMA production experiments , , , , , and it is anticipated that they will become widely used in the production of Fe-SMA. These studies demonstrated the viability of producing Fe-SMAs with improved characteristics for Fe-Mn-Si and Fe-Mn-Al-Ni SMAs. Recent AM technologies used for Fe- SMA are based on laser powder bed fusion (LPBF).
AM can produce parts with higher quality and performance than those produced using vacuum induction melting and other conventional techniques , , . NiTi SMA produced by Electron beam melting (EBM) displayed higher purity than vacuum induction melting manufactured samples . A separate section (6) is designed to analyze all reported studies about the AM of Fe-SMAs to clearly understand how the AM of Fe-SMAs is implemented, the equality of the produced parts, the types of Fe-SMAs that can be produced using AM techniques, and how these technologies can be applied further and generalized for a large number of Fe-SMAs with enhanced properties.
Fig. 6. Production techniques. A flowchart of Fe-SMA production steps. (a) Casting processes. (b) Mechanical alloying. (c) Additive manufacturing.
Preparation Of Fe-Smas
Characterization is a crucial procedure in which several analytical techniques, methodologies, and tools are used to examine, measure, and establish Fe-SMA's chemical, microstructural, and physical properties. Fe-SMA is first produced using either modern processes like AM or more traditional methods including melting/casting and powder metallurgy , , . Further heat treatments are carried out to homogenize Fe-SMA and enhance its properties. Hot forging, rolling, and other shaping methods are applied to the produced Fe-SMA to develop samples with the required geometry and dimensions . The samples required for any characterization technique or test are cut from the as-built Fe-SMA sheets or blocks and machined into the required shape using electrical discharge machining . Inductively coupled plasma optical emission spectroscopy is a typical technique to identify Fe- SMAs’ elemental composition. It is an ionization source that completely breaks down a specimen into its component elements before transferring those elements into ions. It is usually made of argon gas; the plasma is created by "coupling" energy to it via an induction coil , , . Energy-dispersive X-ray spectroscopy coupled with field-emission scanning electron microscopy (FESEM) can also be utilized to investigate the chemical composition of Fe-SMA. Before the microstructural evaluation and conducting the surface analysis, the samples are grounded using SiC sheets having grit sizes of 180-3000 or 400-5000, followed by polishing and etching. A Kalling 2 and Nital are common chemicals used as an etching solution for Fe-SMAs. Polishing is performed using a 50–100 nm colloidal silica suspension neutralized by H2O2 , , .
Fe-17Mn-5Si-5Cr-4Ni-0.3C-1Ti
The SMA was initially melted under a vacuum in an induction melting pot before being cast into a graphite crucible with a cylindrical shape. After casting, the ingot was heat-treated for homogenization. After that, the alloy ingot underwent forging and hot rolling.
Fe-17Mn-5Si-10Cr-4Ni-1(V, C)
Under normal atmospheric settings, the alloy was induction melted and cast into a mold with a diameter and height of 90 and 300 mm, respectively. The ingot was cast using a feeder head and exothermic anti-piping powders to reduce cavities.
Fe-17Mn-5Si-10Cr-4Ni
LPBF was employed to manufacture this SMA. Gas atomization under an Argon environment was used to create the powder. Initial optimization focused on the LPBF processing parameters before producing the final SMA.
Fe-13.51Mn-4.82Si-8.32Cr-3.49Ni-
Induction melting in a vacuum was used. Homogenization was used before the ingot was hot-forged and subsequently hot-rolled. Solution annealing and water quenching were both used to process the rolled samples.
Fe-30Mn-6Si
MA was performed on elemental powders of Fe, Si, and Mn (99.9% purity) in a stainless-steel vial using numerous stainless-steel balls. A planetary ball mill was used to perform the MA. The alloyed powder was then compressed with a compression pressure of 20 MPa and sintered for 10 minutes at 900 °C under a vacuum (2 Pa).
Fe-33Mn-17Al-6Ni-0.15C
The alloy was produced by melting industrial raw materials in an induction furnace with argon gas and then casting it into ingots. These ingots underwent a 24-hour argon-filled homogenization process at
Fe-19.4Mn-5.9Si-9.2Cr-5.1Ni
At the CEIT technological center, powders of the alloy were prepared using gas atomization and sieved before being inductively coupled plasma (ICP) analyzed. The powders were subsequently subjected to laser metal deposition treatment through a KukaKR30 with a ytterbium source using a scanning speed of 665.7 mm/min, laser power of 1150 W, a spot size of 2 mm, and powder flux of 9 g/min.
3.2.2. Surface, phase, and microstructural analysis of Fe-SMAs SEM and optical microscopy (OM) are performed to investigate the surface morphology and the microstructure of Fe- SMAs. SEM and ImageJ software can be used to analyze and measure the volume fraction of the precipitates that are formed in Fe-SMAs . Electron backscatter diffraction (EBSD), a microstructural-crystallographic characterization method based on the SEM, can analyze the microstructure, texture, crystal orientation, grains, phase, or strain of the samples. A perchloric acid and ethyl alcohol electrolytic solution is used to electropolish the Fe-SMA samples before this evaluation. The EBSD data are analyzed using the OIM Analysis™ software. This program can calculate the overall length of a variety of boundaries, such as grain boundaries , , . OM is used in metallographic observation to identify the defects in metals and determine the grain boundaries. Additionally, to differentiate the ε, α', and γ phases using an optical microscope, an optical color etching procedure is applied to the samples in a solution comprising 1.2 g K2S2O5 and 0.5 g NH4HF2 in water. γ phase looks brown, α' is dark, and ε seems white except that thin ε plates show as black lines in color optical pictures , . Using electron channeling contrast imaging (ECCI), the development of the martensite plate during strain is observed in situ .
The ECCI samples were initially ground with SiC sheets up to 4000 grit, polished for about 10 minutes with a diamond suspension (about 3 μm), and then polished precisely with a 50-100 nm colloidal silica liquid diluted by H2O2 . For the identification of the deformation twin in the Fe-SMA, transmission electron microscopy (TEM) can be used.
A twin jet polisher physically grinds and polishes the Fe-SMA specimens in a solution of sulfuric acid and methanol (1:4) to prepare foils for TEM studies . To examine the microstructure of the stress-induced martensite (ε) plates, TEM characterization is also performed . The X-ray diffraction (XRD) equipped with a diffractometer with Cu Kα radiation is performed on samples to examine the phase constituent and crystal structures of Fe-SMAs, where 10% HF and 90% H2O2 solution is used to etch the specimens after mechanically grinding them . Fe-Mn-Si-Cr-Ni SMA samples are electro-polished using a 12.5% perchloric acid and 87.5% ethanol solution to eliminate surface stress before performing the XRD examination . The volume fraction of the different phases in Fe-SMA such as γ-austenite, α′-martensite, and ε-martensite can be estimated using XRD, as well . To obtain the TTs of the Fe- SMA sample, a differential scanning calorimeter (DSC) is used. The instrument is usually standardized for enthalpy and temperature, by considering some samples as standards such as zinc and indium samples , .
Superconducting quantum interference devices are used under fields of 0.05 and 7 Tesla to evaluate the TTs and the thermo-magnetization properties of FeNiCoAlTiNb SMA . 3.2.3.
Shape Memory Testing Of Fe-Smas
To study the SME and damping behavior of Fe-SMAs, DSC and dynamic mechanical analyzer (DMA) can be applied . The bending test for SME is carried out for Fe-SMA samples to evaluate the SME, as shown in Fig.7 (a), and (b). Before measuring the SME, the specimens should be cleaned in a diluted acidic solution to remove the oxidation layer . The procedure of the bending test is first bending the sample to θi = 180 o, keeping the sample in this orientation for a specific time, and then releasing it. After unloading, the sample recovered with angles of θe. Then, the specimen is heated at a specific temperature so the deformed shape will be partially recovered, and the recovery angle θr is measured when the samples are cooled to ambient temperature , . The pre-strain is evaluated using this equation: ε=t/(D+t), where D and t are the bending diameter, and thickness of the specimen, respectively. It is considered the greatest tensile strain at the outside edge of the specimen thickness. The residual strain εr after recovery annealing is then recorded and utilized to determine the strain recovery ratio (SRR), which can be calculated as, SRR=100 × (ε− εr)/ε .
Furthermore, pre-deformation was evaluated by ε = (t/D) × 100 %, where D is the diameter of bending, t is the thickness of the sample, and ε is the pre-distortion . To evaluate the SME using an extension test, a Vickers hardness tester is utilized to generate two indentations on each dog bone specimen's surface. The distance between them, Lo, is then precisely recorded using OM. The separation between the two points on each specimen, L1, is then recorded accurately again after the indented specimens have undergone various degrees of tensile deformation at 293 K (i.e., ambient temperature). Finally, the distance between marked points, L2, is calculated accurately after the distorted specimens have been recovered and annealed at 773 K for 15 min to regain their original shapes. The formula for calculating the SRR is SRR=100 × (L1−L2)/(L1− Lo) . The shape recovery rate η) is determined using η= (θr/ θi - θe) × 100, where θr is the strain recovery angle and θi - θe is the remaining angle after relaxation .
Fig. 7. Testing procedure of Fe-SMA. (a) The procedure of testing and recovery of shape memory property. (b) Schematic diagram showing the evolution of radii during the bending test of the shape memory effect. Table 3. Characterization and testing techniques summary of Fe-SMAs
, , ,
Inductively coupled plasma spectroscopy, energy-dispersive X- ray spectroscopy, spectrometer, X-ray fluorescence
, ,
Electrical discharge machining, Mo filament cutter
Odeling And Simulation Of Fe-Smas
Various studies focused on creating continuum formulations that can predict how SMAs will behave. The continuum state variable models mimic the stress-strain response by using yield functions related to the MT, the evolution of martensite volume percentage, and the associated flow rules , , , , , , . More modeling work has been done to investigate the plastic strain buildup in SMAs. Multi-dimensional empirical models are provided to represent how the plastic and transformational strains evolve under cycling. The driving force of plastic strain agglomeration is the nucleation of slip dislocations at the interface of austenite/martensite when strains and stresses are relatively high, and the main contributing factor in this situation is the slip's critical resolved shear stress , , , , , .
Modeling techniques have also been recommended to visualize the recoverable strains caused by martensite reorientation. By including the dissipation potentials in their derivation, these models combine transformation and martensite reorientation in SMAs to accurately reflect the SME, SE, and deformation of martensite. The twinning stress controls the acquired rules and functions of these models for the martensite reorientation since it has a major impact on the twin interfaces' nucleation and motion, whereas the critical transformation stress governs the yield function of transformation , , . Micromechanical models can also be based on the concept that critical transformation stress is what induces phase transition. To simulate the continuum-shape memory response, these models consider various variant-variant interactions as well as microstructurally informed parameters such as transformation shear magnitudes. These mesoscale formulations concluded that the polycrystalline response is mainly based on the synergy of transformation and slip , , , , .
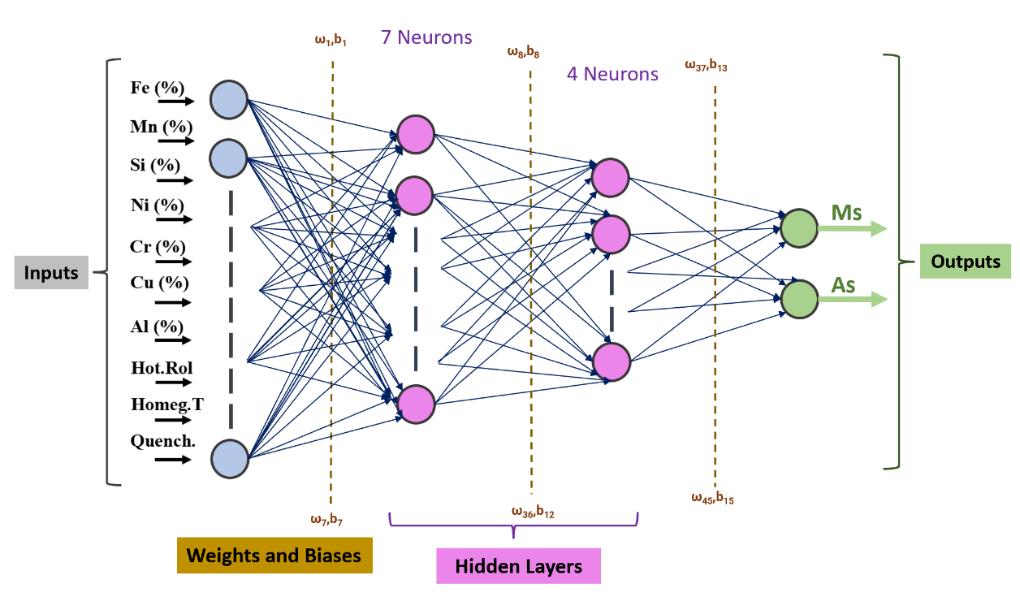
The Modeling of Fe-SMAs starts by determining the TTs. An artificial neural network (ANN) model can be built on a gradient descent learning algorithm to investigate the start temperatures of austenite (As) and martensite (Ms) , as shown in Fig. 8. The model was created, trained, and verified using 85 Fe-SMAs reported in the literature. Ten input parameters were used in the model including the weight percentage of Fe, Mn, Ni, Si, Cr, Al, and Cu as well as hot rolling, quenching, and homogenizing temperature. ANN model can accurately predict the As and Ms temperatures in the range of considered input parameters and can show a strong agreement with the experimental data .
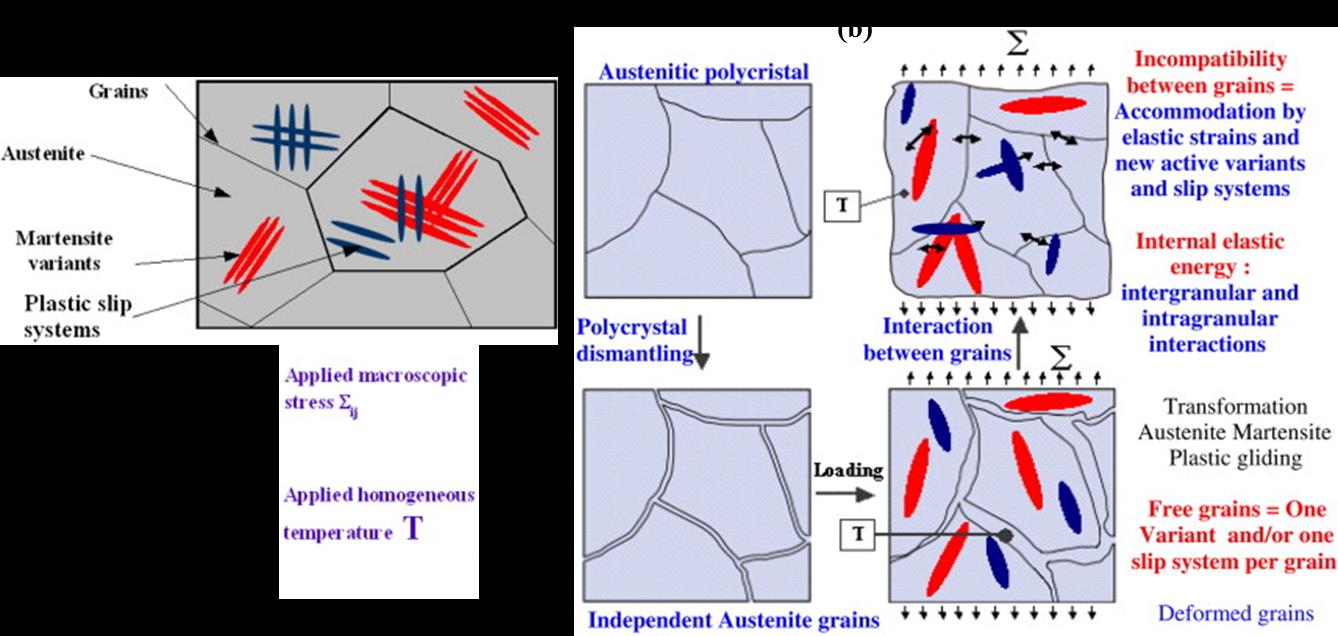
Fig. 8 . Illustration of suggested ANN model of Ms and As temperatures. Additionally, a model was proposed to assess how plastic slip and MT affect the thermo-mechanical behavior of Fe- SMAs . The adopted formulation was established on a condensed micromechanical description. The corresponding homogenous effect was considered on a representative volume element to determine the macroscopic behavior as shown in Fig. 9 (a). The model mainly considered the interactions between the plastic slip and MT mechanisms and their effects (Fig.8 (b)). The concepts of plastic gliding and the martensite volume fraction are introduced as two macroscopic internal variables. The experiments’ validation at different steady temperatures can enable the identification of the material characteristics and the calibration of the suggested methodology for varied homogenous loadings. A good degree of agreement can be achieved between experimental and numerical data .
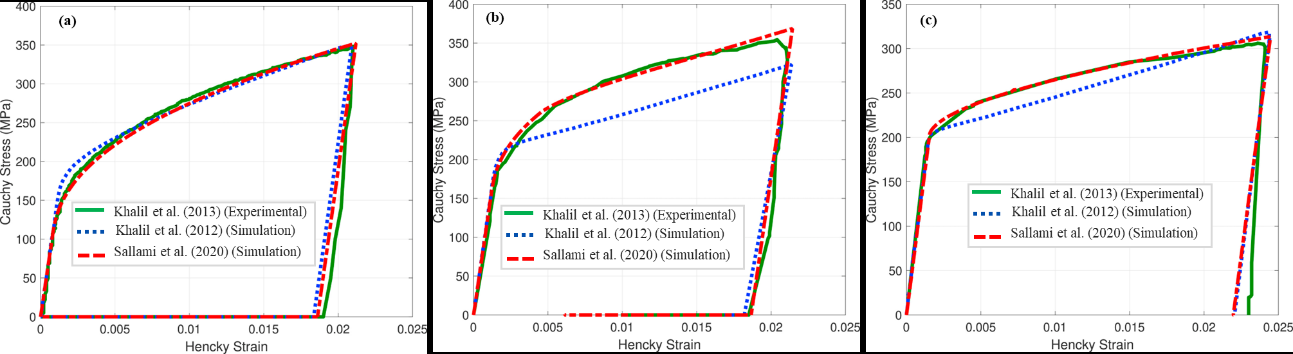
Fig. 9. Representative of volume element and slip interaction. (a) An element of a polycrystalline Fe-SMA is used in the modeling. (b) Interactions between slip systems, martensite variations, and grains . A finite element numerical tool was adapted for a Fe-SMA structural analysis , . Mechanical and chemical variables as well as nonlinear interaction values related to inter- and intragranular incompatibilities were considered during the model derivation. The provided model successfully explained the complicated thermomechanical loading routes. The nonlinear stress-strain graph was precisely simulated and compared to the experiments during loading.
The findings display a strong correspondence with the conducted experiments as shown in Fig. 10. Small-strain thermomechanical models developed to address the link between phase transformation and plastic slip are not appropriate for higher loading. As a result, a finite-strain constitutive model for Fe-SMAs that includes such thermomechanical coupling can be developed . The small-strain model was then expanded within a finite-strain thermodynamic framework to illustrate huge strains primarily brought on by plastic hardening in Fe-SMA. It was created on the concept of a total Lagrangian formulation with a local multiplicative split of the deformation gradient into elastic and inelastic components. The inelastic deformation gradient is also separated into plastic and transformational components .
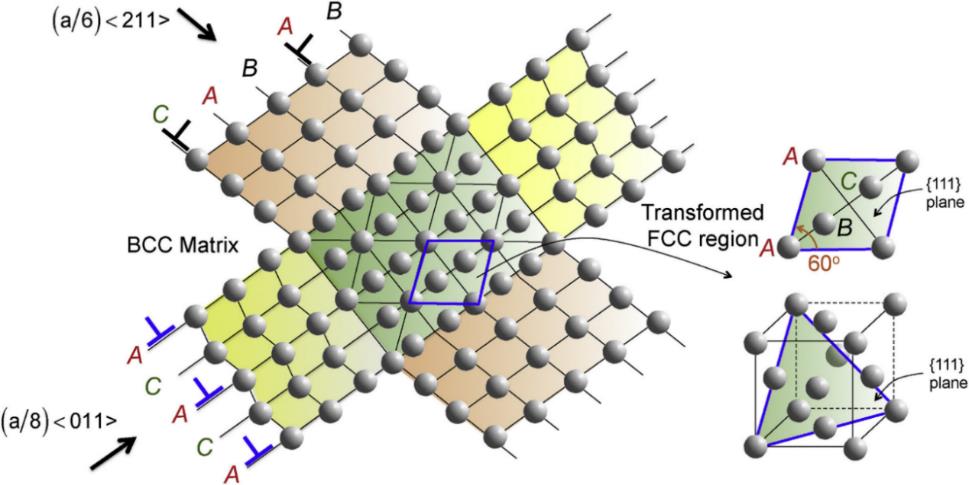
Fig. 10. Simulation and experimental comparison. Simulation compared to experimental results of the stress-strain behavior under tension for Fe-Mn-Si-C SMA. (a) 20 °C. (b) 50 °C. (c) 130 °C . Furthermore, with the help of calculations for double shear in density functional theory, the bcc-fcc transformation in Fe-Mn-Al-Ni SMAs was investigated , as shown in Fig. 11. The dislocations' elastic interactions and transformation shear energy were included in energy expression that was developed to determine the fcc martensite formation stress. It was considered that the bcc to fcc transformation's double shear mechanism is achieved by the movement of two pairs of dislocations, (a0 /8) <110> and (a/6) <112>, on multiple planes in a bcc crystal, the connection of which generates the fcc crystal, shown in (Fig. 11). The stresses for the slip, twinning, and bcc-fcc transformation were reported to be 191 MPa, 201 MPa, and 335 MPa, respectively. These findings were remarkably consistent with the experimental data. The higher slip resistance combined with the low Clausius- Clapeyron slope (dσ/dT = 0.53 MPa/°C, ) of Fe-Mn-Al-Ni alloy was confirmed to be significant for the recoverability of the transformation because the higher slip resistance is required to reduce activation and the number of dislocations at transformation interface. The Bogers-Burgers double shear mechanism is preferred over the "traditional" Bain deformation since it was shown to continue with a substantially lower energy barrier .
Fig. 11. Dislocation-based transformation mechanism considered for the transformation stress modeling in FeMnAlNi
Thermomechanical Properties Of Fe-Smas
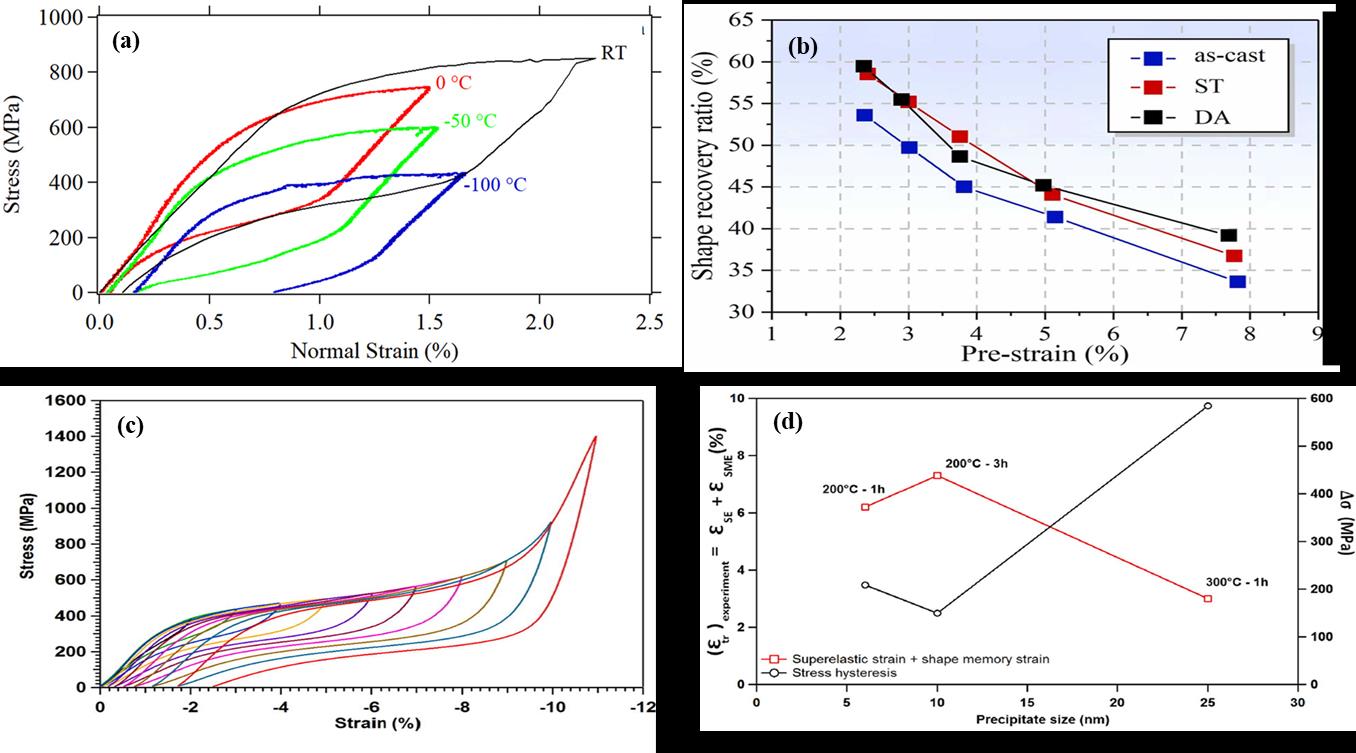
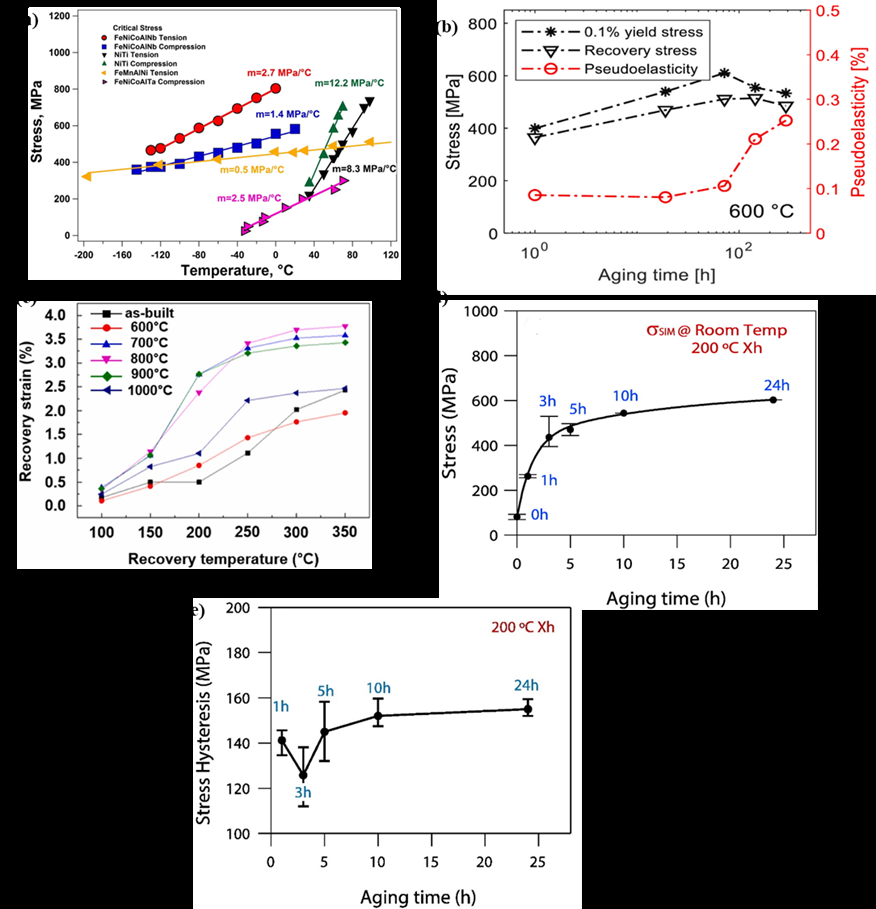
The novelty of Fe-SMAs and other SMAs lies in their capability to experience great deformations and restore their original shape by stress removal (SE) or heating (SME). Phase transformation is the key factor behind these smart properties. Stress-related transformation can result in SE, while temperature-related transformation can produce SME , , . The SME was first observed by Chang and Read in an Au-Cd in 1951. Later, it was reported in numerous NiTi, Cu-based, and Fe-based alloys, which together make up the majority of SMAs. Several Fe-SMAs, including Fe-Ni, Fe-Mn, Fe-Mn-Si, Fe-Ni-Co-Ti, Fe-Pd, and Fe-Pt-based compositions, have been investigated , , . For Fe-Ni-Co-Al-Ti SMA, precipitation heat treatments between 180 and 200 min at 600 °C were favorable for superelasticity with a high degree of recovery (>95%) and significant recoverable strains (7%), as illustrated in Fig. 12 (a). Low-temperature heat treatments changed the strength without producing superelasticity. The critical transition stress being larger than the slip resistance caused this phenomenon, which was attributed to plastic slip . Fe–Mn–Si SMAs have been explored for a long time due to their prospective merits over other SMAs.
These Fe-SMAs possess good weldability, workability, and corrosion resistance, as well as a low manufacturing cost . By adding a particular quantity of Nb and C to traditional Fe-Mn-Si SMAs, the SME is significantly improved, with the generation of NbC precipitates during aging. The pre-rolling or a straightforward extension of austenite just before the aging can further improve SME , , , . It was revealed that the shape recovery ratio of Fe–Mn–Si SMA reduces monotonically with increasing pre-strain as shown in Fig. 12 (a) . This phenomenon is attributed to the buildup of irreversible plastic strain caused by dislocation slip under the influence of increasing pre- strain.
Fe-Mn-Ni-Al SMA has excellent thermomechanical properties and has shown a lot of promise recently , , . It exhibits exceptional superelastic properties such as transformation strains and low thermal hysteresis. It has manifested among the most fascinating SMAs, with a large SE temperature range (> 400 °C). Fe-Mn-Al-Ni SMA displays a considerable work output because of high transformation strains (> 8%) and high transformation stress (500–700 MPa). The transformation stress displays relatively little temperature dependency throughout a wide range of (-196 °C to 240 °C) as compared to NiTi-SMA . The Clausius–Clapeyron slope magnitude (∂σ/∂T) of this Fe-SMA was estimated to be less than 0.2 MPa/°C in compression, and 0.53 MPa/°C under tension. The ∂σ/∂T magnitude is much smaller than that shown in NiTi SMAs (6–8 MPa/°C) , . The mean temperature dependency of the critical stress was estimated to be 0.514 MPa/K in Fe-Mn-Al-Ni while 2.87 MPa/K in Cu-Al-Mn , and 5.87 MPa/K in Ti-Ni . During transformation, an exceedingly modest adiabatic temperature rise of less than 1 °C can be investigated. Fe-Mn-Al-Ni SMAs' SE is governed by a reversible transformation between the bcc and fcc lattices , . Stress must be resistant to temperature changes for SE to be effective. Engineers and scientists can build components and structures with desirable qualities since the critical stress's temperature dependency is easily modifiable. Fe-36Mn-11Al-7.5Cr-7.5Ni was studied and compared to other SMAs in terms of transformation stress and superelastic window, the findings showed that it has extremely advantageous properties , , . The research on Fe-Mn-Ni-Al SMA is expected to expand due to these obvious outstanding functions.
The size, composition, and volume fraction of precipitates were shown to strongly affect the superelastic strain, transformation temperature, stress hysteresis, and critical stress for stress-induced martensitic transformation of Fe- Mn-Al-Ni single crystals. The aging for 3 h at 200 °C produced 7.2% superelastic strain with approximately 6-10 nm precipitate as shown in Fig. 12 (b, c). Increasing the aging time or temperature led to a reduced superelastic recovery because of the growth of coarser precipitates . Fe-SMAs consist of several elements, including Mn, Ni, Co, and Ti, which can be used to modulate flow stresses, TTs, and transformation strains, to enhance their functional qualities.
The addition of aluminum and subsequent heat treatments produces cohesive precipitates, which are essential for SE. Although the precipitations do not change, they do produce internal stress fields that aid in transformation . The nano-scale precipitates can also enhance slip resistance, which promotes martensitic transition and SE. The difficulty of performing reversible SE transformation, especially at ambient temperature, and the destruction of shape memory capabilities with cyclic loading are the main factors that limit SE in Fe-SMAs , , . The pinning of the martensite interface boundary, which prevents perfect reversibility and causes the accumulation of residual strains with sustained loading, has been the main factor contributing to the deterioration of SE properties under functional fatigue . To overcome such limitations, Fe-Ni-Co-Al-X (in which X is either Tantalum, Niobium, or Titanium) and Fe-Mn-Al-Ni alloys , have received a lot of attention recently, and various investigations have found substantial superelastic and recoverable stresses at ambient temperature. Using alloying elements such as titanium, tantalum, and others in Fe-SMAs can improve their thermomechanical properties. They can also enhance other characteristics of Fe-SMAs such as surface roughness as they behave in other materials , , , , , . The Recently investigated Fe-SMAs such as Fe-Mn-Ni-Al SMA can overcome most of the major limitations associated with Fe-SMAs as they offer remarkable properties such as a stable superelastic behavior over a large temperature range and less temperature dependency of the critical stress required for martensitic transformation , , . Table 4 summarizes the functional properties of Fe-SMAs.
Fig. 12. Factors influencing thermomechanical properties of Fe-SMAs. (a) Stress-strain behavior of Fe-Ni-Co-Al-Ti SMA aged for 180 min at 600 °C at various deformation temperatures . (b) Pre-strain effect on shape recovery ratio of Fe- Mn-Si-Cr-Ni SMA at as-cast, solution-treated (ST), δ-annealed (DA) conditions. The recovery annealing was applied for 15 min at 450 °C. (c) Superelastic behavior of Fe-Mn-Al-Ni SMA aged at 200 °C for 3 h. The compression test was performed at room temperature. (d) The effect of precipitate size on the stress hysteresis and superelastic + shape memory strains of Fe-Mn-AL-Ni SMA. (b and c are taken from ).
Table 4. Comparative study of different Fe-based SMAs and their functional properties
Tensile Characteristics Of Fe-Smas
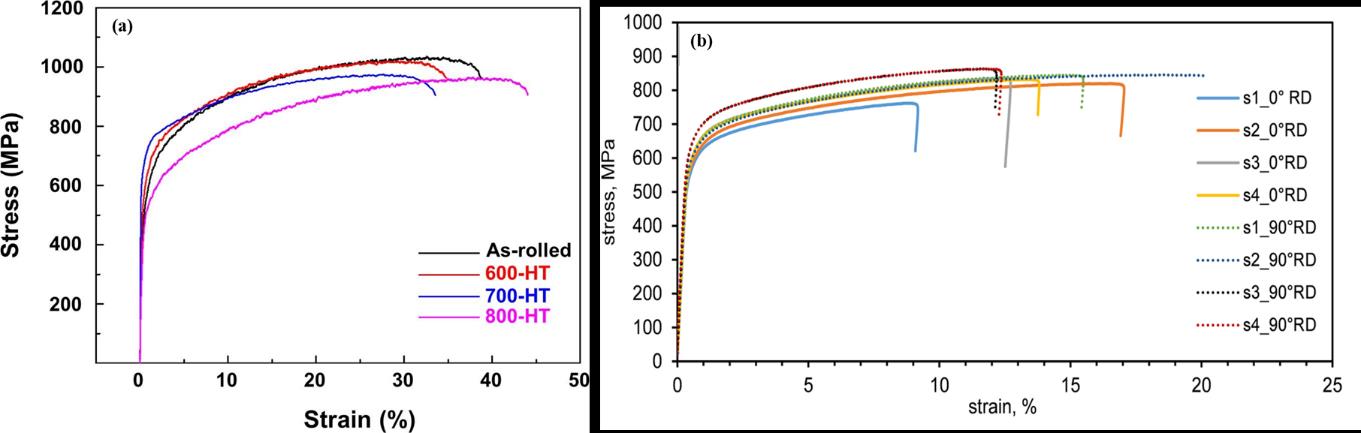
The tensile stress-strain relationship was investigated for Fe-17Mn-5Si-4Ni-5Cr-1Ti-0.3C SMA to evaluate the tensile features . The σ – ε curves of its different tested samples are plotted in Fig.13 (a). The investigated Fe-SMA has a 0.2% proof yield value of 507 MPa and an ultimate extension of 38% in the as-rolled state. When the SMA was aged at temperatures below 700 °C, the yield strength improved, and its maximum stretch reduced with elevating the aging temperature. The textural variations of Fe-SMA during the aging process might be the reason for this phenomenon.
Due to recrystallization, the yield strength significantly decreased when the aging temperature reached 800 °C. Additionally, Fe-17Mn-5Si-10Cr-4Ni-1(V, C) (mass%) SMA was examined, and its elastic modulus was discovered to be between 180 and 185 GPa, which is rather near to that of normal steel (i.e., 200 GPa) . The high fracture strain of this Fe-SMA, which was shown to be over 30% in the absence of buckling while exceeding 8% in the presence of inelastic buckling, indicates that it is incredibly ductile. The yield and ultimate strengths of the unrestrained samples were approximately 400 MPa and 800 MPa, respectively. It was determined that Fe-17Mn-5Si-10Cr-4Ni-1(V, C) (mass%) SMA had a yield strength of 415 MPa when heated to 1100 °C with hot pressing, and 530 MPa when further cold rolled. This rise can be attributed to the last type's smaller average grain size (37 µm) compared to the first one . Fig. 13 (b) displays the hot-rolled Fe-Mn-Al-Ni SMA's mechanical tensile characteristics. The stress-strain graphs show that there is no significant directional dependence. The yield and tensile strength results of the samples obtained parallel to the rolling direction (0° RD) were 585 MPa and 813 MPa, respectively, while they were 625 MPa and 855 MPa, respectively, for those samples produced perpendicular to the rolling direction (90° RD). This is ascribed to the elongated grains in the rolling direction, which finally explains the higher values for yield strength and tensile strength in accordance with the Hall-Petch relation by resulting in a slightly reduced effective grain size perpendicular to the rolling direction The tensile response of Fe-34Mn-7.5Ni-13.5Al SMA under room temperature was tested as shown in Fig.13 (b) and a strain of more than 12% was indicated by the transformation front. At both room temperature and a wide range of temperatures, it exhibits outstanding superelastic performance under tension . The findings of the Fe-17Mn-5Si-10Cr-5Ni (mass-%) SMA study revealed that it has good ductility with a maximum of 55% fracture strain under monotonic stress .
Fig. 13. Tensile findings of different processing cases. (a) Stress-strain findings of aged heat-treated and rolled Fe-17Mn- 5Si-4Ni-5Cr-1Ti-0.3C SMA . (b) Mechanical properties of hot rolled Fe-Mn-Al-Ni SMA in tensile tests of 4 specimens parallel (0°) and perpendicular (90°) to the rolling direction .
Hardness Of Fe-Smas
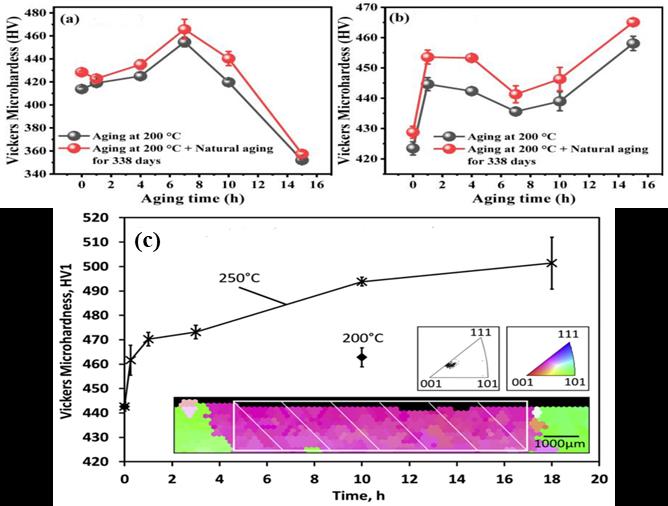
Hardness is an important property of Fe-SMAs and needs to be discussed as suitable hardness demonstrates the capacity of Fe-SMA to withstand erosion, friction, and other types of wear. Fe-36.5Mn-10.7Al-6.2Ni-2.3Mo and Fe- 35.2Mn-10.9Al-7.9Ni-2.4Mo SMAs' microhardness was investigated . Vickers hardness was determined to be 414 and 423 in the solution-treated alloys of Fe-36.5Mn-10.7Al-6.2Ni-2.3Mo and Fe-35.2Mn-10.9Al-7.9Ni-2.4Mo, respectively; however, after 338 days of normal aging, as well as aging at 200 °C for various times, it rose to 428 and 429, as shown in Fig. 14 (a), and (b). The hardness was also evaluated for additively manufactured Fe-34Mn-14Al- 7.5Ni (at. %) SMA . The as-built samples displayed a notably increased hardness compared to those with 1 or 5 heat treatment cycles. In comparison to the earlier study of this work , the hardness in the as-built specimens rose to 420 HV. The Fe-Mn-Al-Ni SMA was subjected to LPBF processing with a preheating temperature of 200 °C to 500 °C, which induced the nanoscale β-phase precipitates and, as a result, generated a higher hardness than solution-treated samples . The hardness of present phases in Fe–Mn–Si–Cr–Ni SMA was modified using samarium . The hardness values of γ and ɛ phases were reported to be 254 and 286 VHN, respectively. Samarium was found to refine the grain size to 15%, which resulted in higher strength. As a result, the hardness has also improved. The development of fine precipitates in Fe-SMAs will reinforce their matrix and hence raise the hardness of the material , , , . Using a 10 h aging at 200 °C, Fe-Mn-Al-Ni single crystals’ hardness with the orientation 〈001〉 rose from roughly 370 HV to 430 HV. A precipitation size of ~ 10 nm after age hardening at 200 °C for 3 h showed the maxim hardness which confirms the substantial correlation between the precipitation size and the microhardness. The Fe-SMA also displayed great pseudoelastic ability under this peak aging environment . Fig.14 (b) exhibits that the aging of Fe-Mn-Al-Ni-Ti SMA at 200 °C for 10 h very slightly increases hardness by about 20 HV1 .
Therefore, aging at 250 °C utilizing varied aging periods was carried out to account for the slower kinetics that was inferred from the suppression of the γ-phase growth in Fe-Mn-Al-Ni-Ti under the air cooling process. After solution treatment, the hardness rose from 440 HV1 to approximately 500 HV1 after an 18-hour aging heat treatment. After 15 minutes at 250 °C, a significant rise in hardness is already achieved, and the gradient becomes less steep as the aging time increases as illustrated in Fig. 14 (b) .
Fig. 14. Microhardness findings of different Fe-SMAs. Microhardness of the 15 °C water-quenched Fe-SMAs. (a) Fe- 36.5Mn-10.7Al-6.2Ni-2.3Mo. (b) Fe-35.2Mn-10.9Al-7.9Ni-2.4Mo. Underwent aging at 200 °C for varying amounts of time before undergoing 338 days of natural aging. . (c) Ambient temperature Vickers microhardness readings in Fe- 34Mn-15Al-7.5Ni-1.5Ti (at. %) after different aging periods at 250 °C. A benchmark hardness value after aging at 200 °C is supplied for comparison .
Fatigue Behavior Of Fe-Smas
The fatigue resistance of Fe-SMA demonstrates its ability to absorb energy under cyclic loads. Fatigue evaluation of Fe-SMA is vital to properly match these materials with suitable applications. The cyclic behavior of the Fe-17Mn- 5Si-10Cr-4Ni-1(V, C) was examined. Fe-SMA's elastic limit (σy,0.2%=371 MPa) was substantially exceeded by the high cycle fatigue and endurance limits. Around 500 MPa marked the shift from high to low cycle fatigue, and 450 MPa was the value when the endurance limit was established to resist more than 2×10⁶ cycles under fatigue loading.
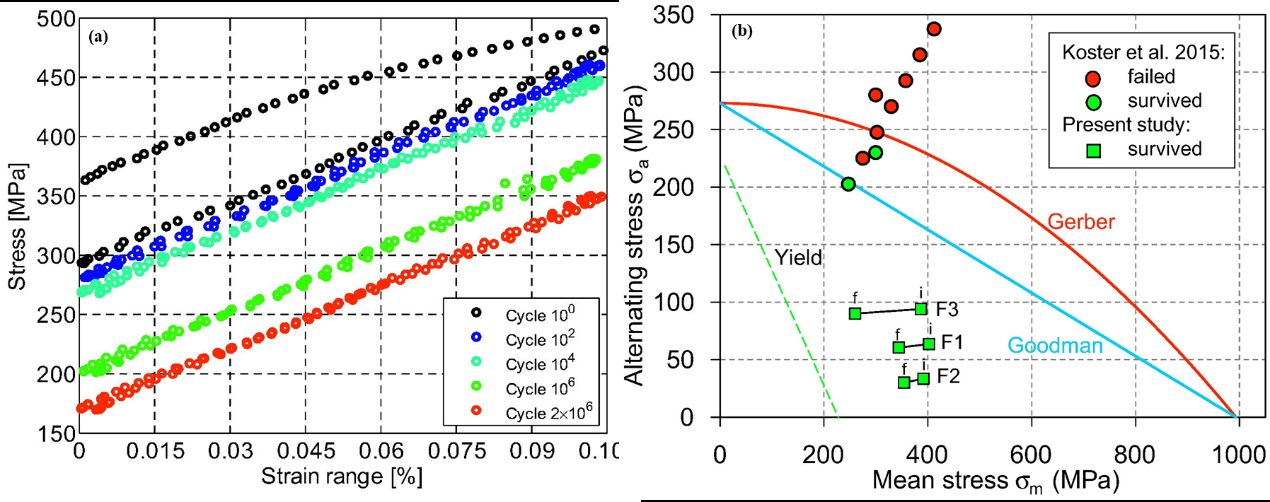
Tested Fe-SMA maintained high fatigue lifetimes even when subjected to maximum stresses that were considerably more than Fe-SMA's elastic limit . The Fe-17Mn-5Si-10Cr-4Ni-1(V, C) SMA fatigue behavior was also evaluated under strain-controlled conditions following pre-straining and thermal activation. The recovery stress was found to decrease under high-cycle fatigue loading, as illustrated in Fig. 15 (a), and this should be included in design evaluations even if the alloy's stiffness remained essentially the same. The reduction in recovery stress was supposed to be primarily the product of relaxation brought on by transformations during cyclic loading. The applicability of using a constant life diagram model to measure the fatigue limit of the Fe-17Mn-5Si-10Cr-4Ni-1(V, C) SMA for various stress ratios was investigated . The current fatigue evaluation findings demonstrated complete agreement with the suggested fatigue design criterion and other reported work as illustrated in Fig. 15 (b). This formulation was presented for a safe design of the Fe-SMA under a high-cycle fatigue loading. The structural fatigue of Fe-34Mn-15Al-7.5Ni-1.5Ti (at%) SMA was conducted at 1% constant strain amplitude. The recovered strains were then saturated at about 1.15% in local residual martensite regions. Global residual stresses increase due to the production of residual martensite in the newly stimulated region. Due to transition occurring in formerly untransformed regions, intermittent augmentation of recoverable strains was investigated. After 2046 cycles, fatigue failure eventually occurred, and the austenite/martensite interface's microcrack initiation and coalescence were found to be the primary cause of this failure. The interfacial dislocations, which are important for Fe-SMAs' SE functioning, always have an impact on the structural fatigue performance since they are the microstructure's weakest link .
Fe-17Mn-5Si-10Cr-5Ni (mass%) SMA results showed that the SMA has excellent low-cycle fatigue resistance for damping applications, meeting the demand for more resilient, long-lasting, and possibly fatigue-free applications in seismically active regions. When the strain amplitude rose from 1% to 9%, the fatigue life was demonstrated to be between 4007 and 83, and the measurements might be 10 times that of typical structural steel. The subsequent damper testing revealed that the fatigue life of the SMA under a rotational angle of 4% was observed to be 173 cycles, as opposed to 16 cycles for its standard steel equivalent, which further confirms the Fe-SMA priority .
Fig. 15. Fatigue behavior of Fe-SMA. (a) The stress-strain behavior of the fatigue-loaded activated Fe-17Mn-5Si-10Cr- 4Ni SMA with a strain range of Δε0 = 0.105%. (b) Findings of the fatigue tests on the Fe-17Mn-5Si-10Cr-4Ni SMA were evaluated using the constant life diagram methodology .
Orrosion Resistance Of Fe-Smas
The correlation between the chemical constituents and oxidation resistance of Fe-Mn-Si-Cr-Ni SMA, while exposed to air at 800 °C, was examined . The more rapid diffusion of Mn, which controls the rate of oxidation, was shown to be possible by an increase in ferrite stabilizer components like Cr and Si in the Fe-SMA at the start of oxidation exposure. The austenite stability must be preserved during the oxidation process to enable the Fe-SMA to function properly . Fe-17Mn-5Si-10Cr-4Ni-VC SMA underwent cyclic oxidation tests at 800, 900, and 1000 °C .
An unusual mass variation was discovered when the mass variation was assessed, and oxide layers were investigated using several characterization methods. After initial spallation, the material continued mass gain, as shown in Fig.16 (b) . On the metal/oxide interface, the created Mn-depleted zone converted the austenite structure into ferrite, and the resultant roughness led to enhanced oxide anchoring. As a result, this alloy is a remarkable alternative for uses where cyclic oxidation is a significant concern . The corrosion performance of this Fe-SMA was compared to that of S500 structural steel, a more common type of steel (EN 10149 PT2 standard) . Fe-SMA was employed as a reinforcement in concrete without experiencing any significant corrosion which confirms that it has higher corrosion resistance than steel S500 . The effect of cerium on the corrosion characteristics of Fe-14Mn-4Si-9Cr-4Ni was examined using anodic potentiodynamic polarization (Fig.16 (a)) and electrochemical impedance spectroscopy in 0.6 M NaCl solution . The findings confirmed that cerium is crucial for improving the corrosion characteristics, while there is a limit to where it starts to be damaging . The investigation of Fe-Mn-Si-Cr-Ni-(Co) SMA further demonstrated that the exceptional protection of passive coatings produced anodically on the SMA in 0.5 M H2SO4 solution is due to a protective layer made of a (Fe, Cr)-mixed silicate . Fe-SMA's high Si content was confirmed to significantly improve Fe-SMA's resistance to intergranular attack in high oxidizing conditions . At 800 °C under air for up to 120 h, the oxidation of a Fe-8.26Mn-5.25Si-12.80Cr-5.81Ni-11.84Co SMA was investigated .
The results demonstrated that exposure to oxidation favors the development of the sigma (σ), chi (χ), and ferrite phases in the support layer. The oxidation pattern followed a parabolic trend, with Mn2O3 oxide formation in the early hours and MnCr2O4 spinel and Mn3O4 growth in the last 24 hours of exposure controlling the oxidation's kinetics .
The corrosion of Fe–Mn–Al–Ni SMA was studied in a 5.0 wt.% NaCl solution . Corrosion characteristics were found to be comparable to those of pure iron. The polarization curves of individual crystals, however, revealed the existence of an unsteady passive system . The Pure Fe and Fe-34Mn-17Al-5Ni SMA's polarization behavior were both examined in NaCl-contaminated Ca(OH)2 and NaCl-free solutions . FeMnAlNi and Fe behaved similarly in the NaCl-free solution and are characterized by strong O2 development at high overpotentials and pronounced passivity at low overpotentials, while the FeMnAlNi SMA exhibited higher pitting corrosion sensitivity than Fe in the NaCl-contaminated solution .
Fig. 16. Corrosion resistance of Fe-SMA. (a) The curves of potentiodynamic polarization for Fe-14Mn-4Si-9Cr-4Ni SMA with different Ce contents in the simulated pore solution . (b) The average weight gain of air-oxidized Fe-8.26Mn- 5.25Si-12.8Cr-5.81Ni-11.84Co SMA at 800 °C .
Anufacturing Cost Of Fe-Smas
The demand for a cost-effective SMA with more economically appealing production pathways prompted the creation of iron-based, or ferric SMAs. This intriguing feature sets them apart from other SMAs. The main reason behind that can be the low price of their constitutive chemical elements including Fe, Mn, Si, Al, and Cr , , . Their cost is reported to be a very small fraction compared to that of NiTi SMAs . Therefore, they have attracted significant interest in the fields of engineering and metallurgy, and they are being thoroughly researched for use in construction where a huge amount of material is needed. The Fe-Mn-Si-SMAs are much cheaper than NiTi SMAs because of the reduced cost of their raw components and their processability in an atmospheric setting. Future costs are anticipated to be like those of highly alloyed stainless steel (about 8–10 €/kg) . A cost analysis was conducted to evaluate the two strengthening options for 6.4 m girders using Fe-SMA and carbon fiber-reinforced polymer . The cost comparison exhibited that both strengthening solutions were observed to be nearly comparable from an economic standpoint when the attainable mechanical clamping systems cost and prestressing force are considered, even though the actual cost of the Fe-SMA strips exceeds that of the regular carbon fiber-reinforced polymer plates .
Alloying Elements’ Role In Fe-Smas
Fe-SMAs’ properties are induced using the reversible transformation between austenite (γ) and martensite (ε) thus, any factor that promotes the austenite-martensite transformation or their reversal can highly boost those properties. On the other side, the variables that hinder such a transition would be detrimental to Fe-SMAs’ properties. The investigation of the various factors impacting the different characteristics of Fe-SMAs is a key factor in easing the choice of the optimum method for enhancing Fe-SMAs’ properties. Alloying elements, precipitate, grain size, texture , grain orientation , , as well as the type of loading (creep, cyclic or constant loading), have all different effects on the MT .
Nickel (Ni), manganese (Mn), chromium (Cr), niobium (Nb), titanium (Ti), tantalum (Ta), cobalt (Co), and boron (B) are incorporated into Fe-SMAs to modify TTs, flow stresses, and transformation strains. Their inclusion into Fe-SMAs with further heat treatments can also produce coherent precipitates that induce enhanced SE. The formed precipitates do produce internal stress levels that aid in the process of transformation , . The incorporation of aluminum (Al) into the FeNiCoAlX system resulted in the development of nanoscale precipitates favorable for SE . SE in Nb-containing compositions was restricted to low temperatures (less than 0 °C), but in the case of FeNiCoAlTi SMA and FeNiCoAlTa SMA , an SE of 7% was displayed at ambient temperature and higher but with quick cyclic deterioration.
Using 10 wt.% of cobalt in Fe–28Ni–6Si SMA with heat treatment at 400 oC for three days, enhanced Fe-SMA’s shape recovery by about 49%. The samples were distorted at −196 °C with a surface strain of 2% and then heated to 1100 °C. The production of martensitic thin plates and the rise in austenite hardness caused by the incorporation of cobalt are the key factors that enhanced the SME . The embedding of Ta into Fe–Ni–Co–Al stabilized the γ′ phase and improved the α′ martensite's strength and tetragonality. However, after aging to produce the γ′ phase, the brittle phase precipitated at grain boundaries, making the Fe–Ni–Co–Al–Ta SMA very brittle. Therefore, a modest quantity of B was incorporated into Fe-SMA to reduce the undesired precipitation at grain boundaries . In addition, β-phase precipitation at grain boundaries with concurrent γ'-phase precipitation inside the grains of systems like Fe– Ni–Co–Al–X (X = Ta, Nb, and Ti) results in a rapid decline in the specimen's ductility and brittle fracture. This phenomenon makes it impossible to examine the SE and SME in these SMAs . Low-boron content of ~ 0.05 at% was embedded in those Fe-SMAs, this modification reduced β-phase precipitation and elevated the SE from 5 to 13% at ambient temperature , , . In Fe-SMAs containing boron, the thermal and mechanical hysteresis was observed larger than in other Fe-SMAs without boron because boron can reduce the Ms temperature and slow down the aging process .
The inclusion of the Ti element was also shown to be beneficial in stabilizing the γ′ phase, with the temperature of γ′ solvus and hardness increased to 888 °C and 420 HV, respectively. Therefore, the Fe–30Ni–15Co–10Al–2.5Ti– 0.05B SMA experienced a thermoelastic martensitic transition with a temperature hysteresis of 31 °C . The use of Nb in the Fe–Ni–Co–Al–Nb–B SMA increased the hardness to around 450 HV due to the stability of the γ′ phase and induced a thermoelastic martensitic transition, but grain boundary precipitation was retained. The grain boundary precipitation can be dramatically suppressed by a small quantity of B . The addition of a modest amount of Nb and C to traditional Fe–Mn–Si SMA significantly improved the SME by causing small NbC precipitates to form during aging. SME can be improved further by pre-rolling austenite before aging treatments , . The inclusion of samarium to Fe–14Mn–3Si–10Cr–5Ni (wt.%) SMA was also observed to enhance the SME by 27% .
Heat Treatment Of Fe-Smas
In Fe-SMAs, heat treatment is frequently employed as a processing technique to homogenize the alloy, change the microstructure, and improve the desired properties. Aging was employed in FeNiCoAlNb SMA to generate nano-sized precipitates to tailor Fe-SMA properties. Fe-SMA displayed strong tension-compression asymmetry and shape recovery of roughly 8.8% in compression and 4.5% in tension after 3 h aging at 700 °C . The critical stress of transformation showed a minimal temperature dependence as shown by the Clausius-Clapeyron curves in Fig.17 (a) . The temperature and time of aging had an impact on the recovery stress, yield stress, and SE of Fe-17Mn-10Cr -5Si-4Ni-1(V, C) (wt.%) SMA . The Fe-SMA displayed increased yield and recoverable stress at relatively moderate aging temperatures (e.g., 600 and 660 °C), as illustrated in Fig. 17 (b). On the other hand, lower yield and recovery stress were observed at higher aging temperatures (e.g., 774 °C). The SE of all aging situations improved after the aging time increased . Fe-34Mn-14Al-7.5Ni SMA was quenched to mitigate intergranular cracking after solution treatment at 1200 °C . Based on changing the quenching procedures, it was demonstrated that regulated γ-phase precipitate at the grain boundary can minimize intergranular cracking without impacting the SE . The impact of heat treatment on the features of additively manufactured Fe-17Mn-5Si-10Cr-4Ni SMA was analyzed .
Heat treatment at temperatures below 800 °C was inadequate to completely accomplish the phase transition from bcc- δ to fcc-γ, whereas heat treatment at temperatures over 800 °C resulted in the thickening and production of new grains in the hcp-ε phase. The latter significantly hindered shape memory . Additionally, σ-phase production using around 3 h heat treatment at 800 °C had a detrimental effect on the SME by altering the chemical makeup of the fcc- γ phase. 800 °C for 0.5 h was shown to be the ideal procedure for achieving a maximum recovery strain as shown in Fig.16 (c) . The influence of aging time on transformation stress and hysteresis was investigated in Fe-34Mn- 15Al-7.5Ni (at%) SMA. The tensile strength at ambient temperature and critical stress for inducing the MT rose without loss of SE with aging at 200 °C . As shown in Fig.16 (d) and (e), the transformation stress rises as the aging time rises, while the hysteresis fluctuates with the aging time. Transformation stress of ~ 600 MPa with a recovered strain of ~ 6.7% was produced after 24 hours of aging at 200 °C . Fe-34Mn-15Al-7.5Ni (at%) SMA was aged at ambient temperature. After 30 days of aging, the MT began at a stress of about 156 MPa, and the deformation was restored after unloading . The superelasticity was ~ 5% which was lower than those aged at 200 °C. The transformation stress increased to 216 MPa after a total of 60 days of ambient-temperature aging. This transformation stress is quite close to those aged at 200 °C for 1 h .
Fig. 17. Heat treatment processing findings. (a) FeNiCoAlNb critical stress for transformation in compression and tension vs. temperature . The Clausius-Clapeyron curves of FeNiCoAlTa, NiTi, and FeMnAlNi are included for comparison , , . (b) Impact of aging time on the thermomechanical characteristics (yield and recovery stress, as well as SE) of FeMnSi-based SMA at 600 °C . (c) Recovery strain vs. recovery temperature of heat-treated additively manufactured Fe–17Mn–5Si–10Cr–4Ni SMA with the same heat-treatment time at varying temperatures , and the effect of aging time at 200 °C on (d) The critical stress for inducing the MT and (e) Stress hysteresis of the Fe-34Mn- 15Al-7.5Ni SMA. Stress hysteresis was evaluated at 3% applied strain in every aging cycle .
Grain And Grain Boundary Effect In Fe-Smas
Grain size control is an important strategy for modifying and promoting the functionality of numerous materials. Grain boundaries must be minimized to achieve decreased creep rates in Ni superalloys or to generate wafers in semiconductors . The reduction of grain size was widely employed in Fe-SMAs to provide exceptional mechanical characteristics, such as increased formability, higher resistance to intergranular cracking, and increased fatigue strength , , , . The grain size control was shown as a key factor to enhance the reversed transformation . The bamboo-like microstructure was shown to be particularly effective in finding good SE and shape-memory abilities , . Grain size has been shown to influence the stability of the constituent phases of martensitic transformations. The decline in grain size exhibited a significant enhancement in the austenite phase stability. This results in a rise in the thermal hysteresis of tiny grains and a drop in MT temperatures , .
The bamboo-like microstructure substantially supports SE in the Fe–Mn–Al–Ni system, demonstrating the importance of grain size in improving desirable characteristics. The SE of the Fe-34Mn-15Al-7.5Ni SMA was found to be significantly influenced by increasing the average grain diameter, width, and thickness of the sheet sample of the relative grain size , , . Large grains with a diameter of several millimeters were shown to be generated using a cyclic heat treatment procedure, and their average size can be regulated by the cycle quantity of heat treatment.
The SE of large grain size samples was enhanced with improved elongation to fracture, lower threshold stress for transformation, and better reversibility . Due to more substantial grain boundary limitations, small grain size results in increased resistance to the superelastic response and reduced reversibility. As grain size increases, grain restrictions lessen, and each grain can change to martensite almost autonomously , , .
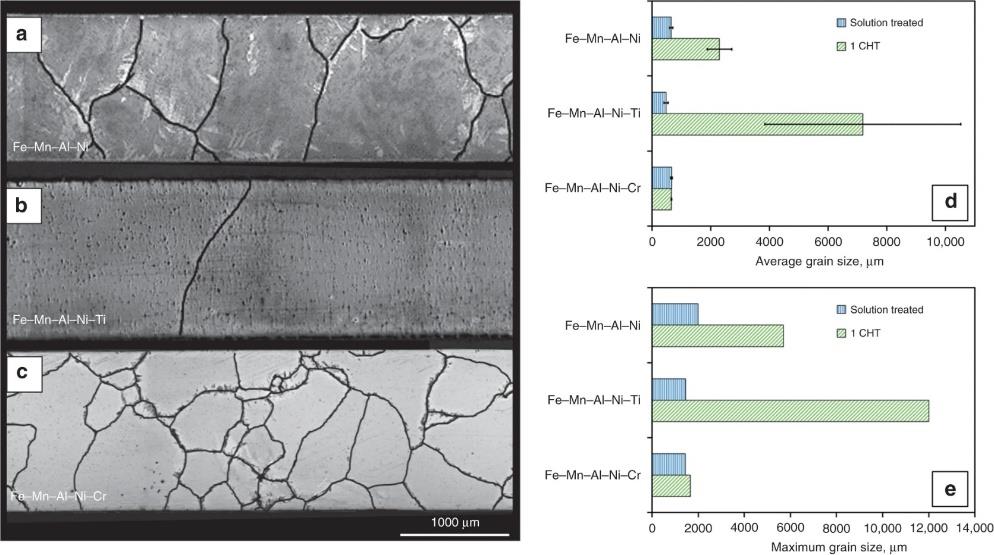
Titanium incorporation into Fe-Mn-Al-Ni SMA was confirmed to overcome its limited recoverability. Introducing modest amounts of titanium into the Fe-SMA significantly boosted abnormal grain growth, because of the high subgrain refinement, as shown in Fig.18 . It is feasible to fabricate bars having large single crystals by tailoring and inducing abnormal grain development. Other systems with comparable microstructural properties can be tailored using this process . Twin boundaries and their effect on strain recovery were investigated in Fe-18.8Mn-5.0Si- 8.5Cr-5.0Ni and Fe-20.2Mn-5.6Si-8.9Cr-5.0Ni SMAs . The presence of Twin boundaries and their interactions can considerably inhibit the gamma (γ) to martensite (ε) transformation. Therefore, after suppressing their formation, an SR of 8.4% and tensile SR of about 7.6% in a cast-annealed sample with coarse grains of around 1.10 mm was achieved.
Fig. 18. Fe-Mn-Al-Ni grain growth behavior assessment. OM images of the typical structure with grain boundaries under one heat treatment cycle. (a) Fe-Mn-Al-Ni. (b) Fe-Mn-Al-Ni-Ti. (c) Fe-Mn-Al-Ni-Cr. (d) Average grain size. (e) Maximum grain size. d and e findings are after solution treatment for 1 h at 1225 °C and one heat treatment cycle .
Effect Of Texture In Fe-Smas
The texture is reported to be an important element in evaluating the SME of polycrystalline Fe-SMAs. The texture is considered the basis for the difference observed in the recovered strain of Fe-SMAs. Modulation of the texture significantly influences both SME and SE features because the transition strain in the crystal is highly reliant on the deformation orientation , . The presence of coincidence site lattice boundaries and low-angle boundaries increases when recrystallization texture is generated by appropriate thermomechanical treatment. Consequently, in polycrystalline conditions, the heavily textured Fe-SMAs including FeNiCoAlTaB and FeNiCoAlNbB had a remarkable ductility exceeding 8% and 20%, respectively. Precipitates’ boundary control was shown to be effective in reducing the grain boundary energy, but no clear connection between grain boundary and precipitation feature has been demonstrated . In FeNiCoAlNbB SMA, the development of cold-rolling and recrystallization textures was illustrated . With the rolling decrease of 98.5% (Fig.19), a rolling texture with a robust brass orientation was improved dramatically. After 1 hour of solution treatment at 1220 °C with a strong {hk0} 〈001 texture, the 98.5% cold rolled FeNiCoAlNbB SMA displayed a good SE of 3.2% with a tensile value of around 960 MPa and residual strain of stability of ~ 0.7%. The significantly improved SE in this Fe-SMA, as compared to the non-SE in the as- forged condition, is primarily due to the development of strong textures and the inhibition of the precipitation in the grain boundaries .
Fig. 19. Texture investigation of Fe-SMA. Orientation distribution functions for recrystallized textures of FeNiCoAlNbB alloy with 98.5% cold-rolling reduction (φ2= 0°, 45°, and 65° sections) . 6. Additive manufacturing of Fe-SMAs: Recent investigations and future trends AM technologies create three-dimensional parts from a digital model by assembling thin layers of materials using a layer-by-layer technique under computer control. This distinctive feature enables the manufacturing of intricate or customized components, eliminating the need for costly tooling, punches die, or casting molds used in traditional processes , . Significant advancements in the constitutive innovations of AM metal processing, such as lower-cost, more reliable lasers, cheaper high-performance computing software and hardware, and metallic powder feedstock tech, have empowered it to be the ultramodern processing method over the last two decades , .
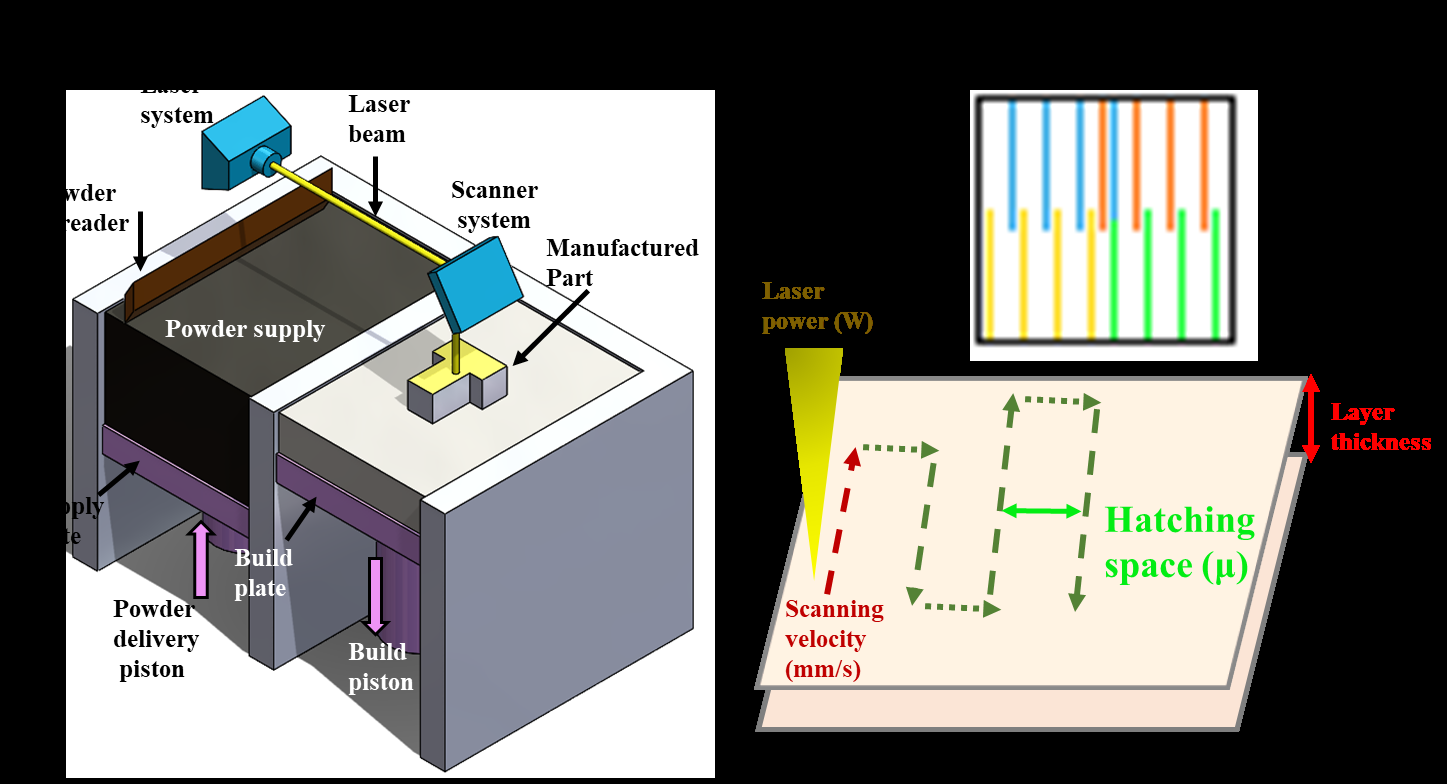
Laser powder bed fusion (LPBF) is a powder bed-based technology that melts and fuses the powdered material utilizing a high-power-density laser as an energy source as shown in Fig. 20 (a). The parameters that should be considered in LPBF processing are the laser power, scanning speed, powder layer thickness, hatching type, and scanning speed as illustrated in Fig. 20 (b). LPBF has been shown to generate near-net-shape objects with a relative density of 99.9% , . It is a more common and most effective printing technique among the various types of AM techniques, such as laser-engineered net shaping, electron beam melting, and wire-arc AM (WAAM), and is typically used for processing most SMAs including Fe-SMAs , , , , , , .
Fe-SMAs fabricated through melting and casting under high vacuum or high purity shielding gas have been the subject of numerous investigations. The final shape is typically obtained through additional machining, such as hot forging and cold rolling, which restricts production to parts with straightforward geometries, such as strips or bars . AM technologies like LPBF and WAAM can offer new ways to get beyond the complexity constraints of conventional manufacture and to fully utilize the appealing functions of these Fe-SMAs. They enable the creation of complicated parts with high densification in a single manufacturing step as the raw metal powder is entirely melted throughout the process .
Fig. 20. A schematic illustrating the LPBF technique utilized in the processing of Fe-SMAs. (a) The LPBF machine's mechanism and parts. (b) The main parameters are optimized to produce high-performance Fe-SMA parts.
Additively Manufactured Fe-Smas
AM of Fe-SMAs has not received much attention until now and appears to be extremely rare, with only a few Fe- SMA systems investigated. Fe–Mn–Si SMAs, among other Fe-SMAs, were shown to be the focus of AM-based research. More details about the recent work related to AM-researched Fe-SMAs can be found in , , ,
, , , , , , , , , , , , , , , , ,
, , , . AM-based studies focused on the LPBF as an AM-based potential process for manufacturing Fe-Mn-Si-based SMAs with promising properties. In recent studies, Fe-Mn-Ni-Si-Cr SMA was first manufactured using LPBF. The aim of the research was to use a processing window of 115 W – 175 W combined with a scanning speed of 300 mm/s – 600 mm/s to achieve a high- densified Fe-Mn-Si-based SMA . Fe-Mn-Si-based cubic samples of 10x10x10 mm3 were fabricated to investigate the densification and microstructural behavior of the SMA. The highest-density material was then used for mechanical and thermomechanical investigation. The study showed that the used powder had a chemical makeup of Fe-17Mn- 5Si-10Cr-4Ni (wt.%). The results of the powder investigation indicated that the particles were mostly spherical, with a mean particle diameter of 29.7 µm and a size distribution range of 10–50 µm , , . To identify the optimal conditions necessary for printing Fe-Mn-Si components with enhanced properties, tensile and intricate shape specimens were printed at varying scanning speeds, laser powers, build orientation, as well as constant hatching space, and layer thickness. The specimens printed with high volumetric energy density (VED) showed minimal defects including lack of fusion, contour, and cracks defects compared to other parts with lower VEDs. Higher VEDs also produced the best densities and porosities , , . Fe-Mn-Si SMA was also used to fabricate intricate 3D structures utilizing LPBF . Successful fabrication of a completely working Fe-SMA with remarkable mechanical qualities was accomplished. Yield stress of ~ 230 MPa with an elongation of ~ 50% was attained by a 30-minute straightforward heat treatment at 800 °C following LPBF processing. This strength was at least three times greater than the greatest value for shape memory polymers that have ever been recorded (70 MPa). Heating the deformed samples at 200 °C achieved a shape recovery of ~ 36% and ~ 47% in the parallel and perpendicular directions to the building direction, respectively .
The impact of post-heat treatment on the characteristics and microstructure of additively produced Fe–17Mn–5Si– 10Cr–4Ni using LPBF was examined . It was found that using a temperature less than 800 °C was insufficient to fully perform the bcc-δ to fcc-γ transformation, but temperatures over 800 °C resulted in grain expansion and hcp- ε phase thickening, which had a significant impact on SME. σ-phase production via ~ 3 h heat treatment at 800 °C had a detrimental effect on the SME by altering the chemical constituents of the fcc-γ phase. The SME parallel to the fabrication direction was higher than that parallel to the laser scanning direction and 45° to the scanning direction. In contrast to the random but weaker {111} and {100} textures that were seen in the scanning direction and 45 with the scanning direction, the higher SME parallel to the fabrication direction was attributable to the texture {110} in the plane perpendicular to the fabrication direction . Additionally, Fe-Mn-Al-Ni SMA was processed using LPBF with a high-temperature build plate of 500 °C to overcome constraints associated with the crack formation during AM . Increased diameter in the as-built samples led to a strong texture in the 001> direction and a columnar-grained microstructure. An increased hardness was observed in as-built samples as well. The treated alloy's applied cyclic heat treatment induced abnormal grain development as well. Last but not least, tensile load testing showed an identified stress plateau and reversible strains of approximately 4% . The Fe-Mn-Si-Cr-Ni SMA was also fabricated using LPBF under a high energy density of 222–250 J/mm3 . The Fe-SMA achieved a combination of a high strength of over 480 MP, good ductility of about 30%, superior ultimate tensile strength of higher than 1 GPa, and a significant recovery strain of roughly 6%. The strain and shape recovery findings are summarized in Fig. 21. Fe-Mn-Al-Ni SMA was another system processed using LPBF . Temperature variations and solidification speed, and therefore processing variables including the actual specimen design, had a significant impact on the microstructural development during processing. A noticeable grain growth was started by a single-step heat treatment, which produced microstructures with good reversibility. The greatest reversible strain, as determined by the stress-strain response, was 7.5% . The summary of AM-based processing parameters, powder characteristics, and sample specifications is provided in Table 5.
Fig. 21. Shape memory characteristics of the LPBF-fabricated Fe-Mn-Si-Cr-Ni SMA. (a) The impact of deformation temperature on shape recovery ratio and recovery strain in the specimen manufactured with an E of 250 J/mm3 after 5% bending. (b) Recovery strain after 5% bending at 77 K and room temperature in the specimen produced with varying energy input. (c) Shape recovery ratio and recovery strain at room temperature as a function of the fabrication's varying energy input. (d) Shape recovery ratio and recovery strain at 77 K as a function of the fabrication's varying energy input .
Table 5 Processing parameters and specifications of AM-produced Fe-SMAs
Waam
Wire feed speed of 3 m/min, travel speed of 480 mm/min, voltage of 18V, contact tip to work distance of 10 mm, shielding gas of 82% Argon and 18 CO2, and gas flow rate of 15L/min.
Structure
DED, directed energy deposition; d50; mean diameter of powder particles, H, hatching space; L, layer thickness; LPBF, laser powder bed fusion; P, laser power; VED, volumetric energy density, V, laser scanning speed; WAAM, wire arc additive manufacturing. 6.2. Features and limitations of additively manufactured Fe-SMAs The research on Fe-SMAs such as Fe–Mn–Si SMAs has mainly centered on the microstructural and thermomechanical characteristics of conventionally manufactured parts. Various microstructures and textures, as well as different shape memory properties, are believed to be achieved using the LPBF technique . Since the SME is achieved using fcc-γ → hcp-ε transformation and its reversal , , the as-built additively manufactured specimens with optimum LPBF parameters were heat treated for 30 min at 800 °C to achieve an austenitic phase and melt any ferritic phase produced in the rapid consolidation . After annealing, high elongation, strength, and ductility were exhibited. The SME and SE were obtained, which were higher than those observed in the conventionally produced Fe–17Mn–5Si–10Cr–4Ni-1(V, C) . SME and SE were significantly dependent on the build direction compared to the loading direction. Strain recovery was enhanced when both loading and building were in a parallel direction, this is due to the increase of (101) orientated grains . After being heat-heated at 200 °C and then cooled, the restored strain of the tensile specimens including horizontal and vertical samples elongated to about 4 % strain as illustrated in Fig. 22 (b) . The mechanical and thermomechanical findings of the LPBF-generated FeMnNiSiCr SMA are summarized in Fig. 22. Successfully created complex structures that had dramatic shape recovery, good dimensional precision, and complex geometry. After deformation and subsequent heating, as seen in Fig. 22 (e), shape changes take place. Every object tested exhibits a clear restoration of the original printed shapes after heating, which is attributable to the back MT. Additionally, the Fe-Mn-Al-Ni process employing the selective laser melting technique demonstrated outstanding features. Temperature changes and solidification speed, and therefore processing variables including the actual sample shape, had a significant impact on the microstructural evolution during processing. Heat treatment caused strong grain development through single step solutionizing, which produced microstructures with good reversibility. The maximum reversible pseudo-elastic strain was found to be around 7.5 % based on the alloy's compressive stress-strain response , . In-situ digital image correlation combined with EBSD was performed to investigate the phase distribution within differently oriented grains of Fe–17Mn–5Si–10Cr–4Ni SMA . It was applied after deformation at 2% Fig. 23 (b) and 4% Fig. 23 (c) while the EBSD (Fig.23 (a) was applied prior to deformation. The digital image correlation analysis demonstrated the localization of the strain, which indicates that the strain was accommodated by the emergence of slip, martensitic transformation, and stacking faults . Different grains were analyzed to have different strain distributions and concentrations of stacking faults (Fig. 23 (d)). It was concluded that the grains with 〈1 1 0〉 orientation along the loading direction were preferred for the martensitic transformation and resulted in more pronounced work hardening as well as improved shape memory properties.
A common challenge in LPBF technology is that the processing parameters must be optimized to minimize defects and produce specimens with higher quality. Several defects including keyholes, lack of fusion, cracks, irregular voids, and spherical gaseous pores are likely to arise in additively manufactured specimens, resulting in low-density parts with degraded mechanical and functional properties. The reason for the development of such defects is the fabrication of the samples at processing parameters that are far from the optimal window , , , , . The concentrated heating and rapid cooling along with using powdered material as the feed establishes a favorable environment for porosity formation by leaving cracks, partially melted powder, lack of fusion zones, or generating gas bubbles . A lack of bond formation between the scanning tracks and layers will result in the creation of voids if the powder does not melt completely and the melt pool fails to penetrate far enough into the previously solidified layers . Cracking has been investigated to occur when parts are manufactured with a low specific energy density. The fundamental reason for crack generation is excessive levels of the bcc- δ phase, which is exceedingly brittle comparable to fcc-γ, as well as the residual stress and surface roughness caused by a significant temperature differential around the laser spot , , .
Cracks typically form and propagate near the sample's edge, in which the surface roughness functions as a stress concentration source known as the residual stresses, and the notch effect is relatively high. For high-energy-density samples, on the other hand, the high ratio of power to scanning speed results in increased penetration depth and melt pool size, as well as a drop in molten material viscosity. Throughout the deposition, great track bonding, as well as suitable wetting, distributing, and flattering features of the melted tracks, are promoted, ensuring the production of dense bulk elements. Because the fcc-γ phase has higher ductility than bcc-δ, the predominantly austenitic microstructure resists cracking , . Preheating at a suitable temperature and post-heat treatment processing are two common strategies used to minimize cracking in additively manufactured Fe-SMAs , .
Fig. 22. LPBF findings of Fe–17Mn–5Si–10Cr–4Ni SMA. (a) Recovery strain as a function of temperature after 4% pre- straining for LPBF FeMnNiSiCr SMA in both horizontal and vertical orientations. (b) Cyclic loading-unloading curves. (c) Superelastic strain and hysteresis width vs. the applied stress. (d) Testing the SME of Fe-based 3D-printed complex shapes at 300 °C after deformation, (1,2) is defined as type I, while (3,4) is known as type II .
Recently, the effect of in-situ preheating, in-situ heat treatment, or post-heat treatment on AM-produced Fe-SMA has been investigated, , . The impact of two different post-heat treatment settings on the mechanical, microstructural, and shape memory characteristics of a Fe-17Mn-5Si-10Cr-4Ni-(V, C) (wt%) SMA produced using LPBF was explored . Specimens aged following solution treatment at 1050 °C for 2 hours revealed fully crystallized equiaxed grains with annealed twins, while specimens aged immediately at 750 °C for 6 hours from the as-built condition had elongated fcc-γ grains with a substantial quantity of low angle boundaries, as illustrated in Fig.
24. The as-built and direct aged samples had average fcc-γ grain sizes of around 10 and 30 μm, respectively. Thus, substantial grain growth occurred throughout the direct aging process.VC precipitates were finer and more evenly distributed in the direct aging than in the aging after the solution heat treatment. Moreover, the solidification cell structure was preserved in the direct aging since the VC precipitates were primarily generated along the margins of the solidification cells. Similar recovery strains and superelasticity were displayed by both conditions. Conversely, the direct energy exhibited significantly higher yield strength and recovery stress in comparison to the aging after the solution heat treatment. The fine consolidation of structures and fine distribution of VC precipitates in the direct aging followed by quick solidification of the LPBF technique could be attributed to the higher yield and recovery strains in the direct aging compared to the aging after the solution treatment.
The effect of in-situ treatment on the bcc- δ formation in LPBF-produced Fe-Mn-Si SMA and its transformation into the fcc- γ phase was explored . To apply the in-situ treatment, the alloy was manufactured utilizing a laser power range of 380–420 W. Throughout the manufacturing process, each layer was subjected to additional laser scanning with the same laser power. The δ phase transforms into the γ phase by increasing the laser power from 380 W to 420 W, with the maximal transformation occurring at 400 W. The sample produced at 420 W has an almost entirely fcc- γ microstructure (γ of ~ 93%). Investigations were conducted on the microstructure of the laser-rescanned areas.
Compared to other areas, the rescanned area had a much lower bcc-δ phase fraction. On considering this, the additional bcc-δ to fcc-γ phase transformation that the laser remelting effect causes in this area can account for the comparatively low bcc-δ fraction in the rescanned area.
Fig. 23. Digital image correlation of LPBF-fabricated Fe-Mn-Si SMA. (a) EBSD map with IPF coloring associated with the loading direction. (b) Strain maps were obtained at a deformation of 2 %. (c) Strain maps were obtained at a deformation of 4 %. d | strain and EBSD maps for the three chosen grains. The red arrows represent the hcp-ε lamellae nucleation along these planes .
Authors:
Peder EZ Larson 1, 2,* , Jenna ML Bernard1, James A Bankson 3, Nikolaj Bøgh 4, Robert A Bok1, Albert P. Chen 5, Charles H Cunningham 6,7, Jeremy Gordon1, Jan-Bernd Hövener 8, Christoffer Laustsen 4, Dirk Mayer 9,10, Mary A McLean11 12, Franz Schilling13, James Slater1, Jean-Luc Vanderheyden5, 14, Cornelius von Morze 15, Daniel B Vigneron1, 2, Duan Xu1, 2, and the HP 13C
94143, Usa.
Denmark. 5 GE Healthcare, Menlo Park, California, USA. 6 Physical Sciences, Sunnybrook Research Institute, Toronto, Ontario, Canada.

8 Section Biomedical Imaging, Molecular Imaging North Competence Center (MOIN CC), Medicine, Baltimore, MD, USA. Cambridge, United Kingdom.

14Jlvmi Consulting Llc, Dousman, Wi, Usa
#See Acknowledgements for a list of all HP 13C MRI Consensus Group Members This work was supported by the ISMRM Hyperpolarized Media MR Study Group, the ISMRM Hyperpolarization Methods & Equipment Study Group, and the Hyperpolarized MRI Technology Resource Center (NIH/NIBIB grant P41EB013598).

Abstract
MRI with hyperpolarized (HP) 13C agents, also known as HP 13C MRI, can measure processes such as localized metabolism that is altered in numerous cancers, liver, heart, kidney diseases, and more. It has been translated into human studies during the past 10 years, with recent rapid growth in studies largely based on increasing availability of hyperpolarized agent preparation methods suitable for use in humans. This paper aims to capture the current successful practices for HP MRI human studies with [1-13C]pyruvate - by far the most commonly used agent, which sits at a key metabolic junction in glycolysis. The paper is divided into four major topic areas: (1) HP 13C-pyruvate preparation, (2) MRI system setup and calibrations, (3) data acquisition and image reconstruction, and (4) data analysis and quantification. In each area, we identified the key components for a successful study, summarized both published studies and current practices, and discuss evidence gaps, strengths, and limitations. This paper is the output of the “HP 13C MRI Consensus Group” as well as the ISMRM Hyperpolarized Media MR and Hyperpolarized Methods & Equipment study groups. It further aims to provide a comprehensive reference for future consensus building as the field continues to advance human studies with this metabolic imaging modality.
Keywords: Hyperpolarized MRI, metabolic imaging, carbon-13, pyruvate, dissolution dynamic
Introduction
MRI with hyperpolarized 13C agents, also known as hyperpolarized (HP) 13C MRI, has shown great potential as a novel imaging modality, particularly for its ability to probe metabolic processes in real time. The first human studies with HP [1-13C]pyruvate were performed in 2011 in prostate cancer patients (1).
Since then, there have been over 60 papers published with imaging results of human subjects from 13 different sites, with applications including prostate cancer, brain tumors, breast cancer, kidney cancer, pancreatic cancer, metastatic disease, liver disease, ischemic heart disease, diabetes and cardiomyopathies. The vast majority of these studies used [1-13C]pyruvate (1–63), where [2-13C]pyruvate (64) and 13C-urea (56) have been demonstrated too.

As clinical HP 13C MRI advances, there is a growing need to build consensus for best practices, which are critical for comparing data across sites, performing multi-site trials,deploying methods to new sites, partnering with vendors, and potentially for obtaining broader regulatory approvals.

In March 2022, we initiated an effort to build consensus within the HP 13C MRI community with this opportunity in mind, and it was greeted with strong enthusiasm. The “HP 13C MRI Consensus Group”, containing over 55 members from 27 sites, identified the area of greatest need and opportunity for consensus building to be HP [1-13C]pyruvate human
●
Pyruvate is the most mature and widely used HP agent and has the most significant translational evidence emphasizing the potential clinical impact.
●
Clinical trials, particularly multi-site trials, have the strongest need for consensus methods to ensure that data can be combined across sites. This work is a Position Paper for which the goal is to describe current successful practices and study methods for HP [1-13C]pyruvate human studies along with justification to support those practices. This is divided into four major topic areas: (1) HP 13C-pyruvate preparation, (2) MRI system setup and calibrations, (3) data acquisition and image reconstruction, and (4) data analysis and quantification (Fig. 1). The current successful practices and study methods include a literature review of published peer-reviewed journal papers showing human HP [1-13C]pyruvate study data, up to September 2022 (1–63), as well as new unpublished information from surveys of HP 13C study sites. Based on this information, we also highlight the evidence gaps, strengths, and limitations of current practices which are summarized at the end of each section.
Figure 1: Illustration of the HP 13C MRI human study process, including the 4 major areas covered in this paper: Hyperpolarized 13C-pyruvate preparation, MRI system setup and calibration, Acquisition and Reconstruction, and Data Analysis and Quantification.

Figure 2: Anatomical targets of HP [1-13C]pyruvate MRI human studies published up to September 2022.
Hyperpolarized 13C-Pyruvate Preparation
This section covers the processes for creating the HP agent, 13C pyruvate, and will include many aspects and considerations that are needed to safely and effectively prepare doses for metabolic imaging studies in human subjects. These include material, personnel, equipment and facility, fluid path preparation, quality control, and release.

It is helpful to understand that the specifications of a dose of 13C pyruvate suitable for in vivo MR HP metabolic imaging were shaped in part by early preclinical studies performed by GE HealthCare summarized in Ref. (65). In short, the safety of the two novel drug components, 13C pyruvate and the electron paramagnetic agent (EPA) AH111501, were demonstrated in those studies. The more precise formulation of the dose suitable for human use was then determined from clinical studies (66) that included two Phase 1 clinical trials in young and elderly healthy volunteers without hyperpolarization of the 13C nuclei and another Phase 1/2a dose escalation and imaging feasibility study with HP 13C pyruvate in 31 prostate cancer patients at the With the exception of the first HP 13C imaging clinical trial, which utilized a prototype device in a cleanroom (1), all HP 13C studies performed in humans to date have utilized the SPINlab polarizer (manufactured by GE HealthCare). Consequently all doses of the HP 13C pyruvate delivered by SPINlab have been produced using the “SPINlab Pharmacy Kit” that serves as the container-closure system for the various drug components (13C pyruvic acid and EPA mixture, dissolution medium, and neutralization and dilution medium) during sample polarization, dissolution and quality control (QC) processes. Thus many aspects of the HP sample preparation considerations discussed below are related to the SPINlab instrument and the consumables designed to be used with it (67).
General Considerations
While more than 860 patients or healthy subjects having been injected with HP 13C pyruvate as of January 2022 without reports of any serious adverse events (68), HP 13C pyruvate injection remains an investigational MR contrast agent and can only be administered by those with Investigational New Drug (IND) exemption from the Food and Drug Administration (FDA) in the USA, a Clinical Trial Application (CTA) in Canada, approval from National Research Ethics Committee Services in the UK, or approval from the relevant local regulatory body. Thus, methods and processes involved to produce a dose should have patient safety as the first priority. Since utilizing dissolution dynamic nuclear polarization (dissolution-DNP) for human use is still a relatively new development, there are no existing published regulatory guidelines specifically for this method.
There are two major production styles that determine how various sites approach the agent preparation. In the US, the most common approach is to rely on a sterilizing filter (“Terminal Sterilization”) to ensure sterility of the final product, akin to PET tracer production, where a starting molecule with a radioisotope is processed using various other ingredients to make the final, desired and injectable contrast agent within a necessarily short amount of time (69). For these sites, sterilization of the components and accessories upstream of this filter are not required, although many of them were manufactured and tested following Good Manufacturing Practice (GMP) or Good Laboratory Practice (GLP) requirements. The filling process is usually performed under an ISO 5 laminar flow hood, but a clean room or an isolator is not required.
This approach is typically accompanied by testing the integrity of the sterilizing filter prior to release of the dose for injection. Typically, post release endotoxin and sterility tests are performed using an aliquot reserved from each released dose.
In the UK and EU, the most common approach is to more-closely follow sterile pharmaceutical compounding guidelines (70), where all components and ingredients are required to be sterile or manufactured under GMP guidelines and are assembled and filled within a clean room environment or an isolator system (“Sterile Preparation”). Typically a batch of Pharmacy Kits for HP 13C pyruvate injection are prepared together. The sterility of the final dose is also ensured by batch validation testing, in addition to the sterility of the ingredients and the sterile compounding process. The endotoxin and sterility testing are performed for the process validation but are not performed for each injected dose.
Some institutions fill and assemble the Pharmacy Kit required for a specific study on the same day or the day prior to polarization, dissolution, and patient administration, but others have also demonstrated the feasibility of preparing a batch of kits, keeping them in a -20ºC freezer and using them over a period of a few months.
Beyond the obvious requirements that the process and the facility has to ultimately produce a dose that is safe to inject into a human, regulatory authorities will also focus on the question “Are you in control of your processes?”. To be in control of your process requires an in-depth and broad understanding of all processes involved in pre, post, and during the production process.
Personnel
It is typical and may be required to have licensed personnel involved in the production process depending on local regulations.Typically a pharmacist, radiopharmacist or other similarly qualified person (QP), in charge of the facility where the Pharmacy Kit filling and preparation is taking place, is responsible for the overall process and the release of the injectable dose.
Qualified cleanroom technicians are often involved in the Pharmacy Kit filling under the supervision of the pharmacist or QP. As is required for pharmaceutical compounding or PET tracer production, training requirements and training records for all personnel need to be maintained and available for audit by the FDA or equivalent.
Equipment And Facility
The facility and all equipment need to have standard operating procedures (SOPs) that describe how equipment is used, maintained, and calibrated to comply with relevant legislation. Currently, almost all the filling of the Pharmacy Kit takes place within a compounding laminar flow hood or isolator (typically ISO 5). At some sites, the filling is conducted within a cleanroom, while at others, it is conducted in a dedicated non-cleanroom space, reflecting differences in cleanroom approach and specifications between regulators worldwide (71). Some equipment or facilities, such as the compounding hood or cleanroom, may require external certified laboratories for testing.
Material Handling
Material handling guidelines (69,70) require SOPs detailing a system to track all of the materials involved in the HP production process for a particular patient dose, similar to current good manufacturing practice (cGMP) requirements for material handling for drug compounding. This includes acceptance standards, storage conditions, amount used in the patient dose for each ingredient and materials used in the assembly of the fluid path and Pharmacy Kit. Currently some users choose to open and inspect and sometimes modify the Pharmacy Kits upon arrival, but some users keep them in the sealed packaging until they are required for dose preparation.
Pharmacy Kit Filling And Assembling
As required by an IND or its equivalent, the preparation of the doses of HP 13C agent are detailed in the Chemistry, Manufacturing, and Control (CMC) section of an applicable regulatory submission; an example of this has been made available (72). It describes the processes of filling the Pharmacy Kit with the different components that make up the final drug product, and of assembling the final kit for either storage or immediate use in the polarizer. Special attention should be given to the laser welding process in order to satisfy installation qualification (IQ) and operational qualification (OQ). Typically, the final developed process is validated by process qualification (PQ) runs, during which 3 or more Pharmacy Kits are filled and used and the final HP 13C products are tested for endotoxin and sterility and to confirm that they meet the dose specifications for injections (usually including pyruvate concentration, residual EPA concentration, pH, liquid state polarization level and dose temperature). The data from 3 consecutive PQ runs are submitted as part of the IND submission (or its equivalent), and are often also reviewed by the Institutional Review Board (IRB) where the studies are conducted.
Quality Control And Dose Release
The quality control (QC) and dose release can be separated into two aspects: one is the QC and release of the filled Pharmacy Kit, and second is the QC and release of the HP 13C agent for injection, after polarization and dissolution. For institutions filling a batch of kits and storing them to use over a period of time, typically the batch can be released based on initial validation, environmental monitoring data from the day of kit production, and if filters are used during preparation of any of the components, filter integrity testing. But in some cases one or more kits are used for validation before the batch of kits are released for future use. For institutions that fill only the kits required for specific studies shortly before the experiment, the filled kits often do not go through separate release tests before they are used.
The quality control of the HP 13C pyruvate solution post dissolution is primarily performed to ensure that the agent meets the dose specifications (Table 1) before it is administered to the subject. These specifications target both safety (pH, residual EPA, temperature) and efficacy (pyruvate concentration, polarization, volume). Typically, the pyruvate concentration, residual EPA concentration, pH, dose temperature, dose volume, and liquid state polarization are measured by the QC accessory associated with the SPINlab polarizer. Some users perform a secondary measurement for one of the parameters, such as pH, using a different instrument or pH paper. For sites that do not go through a separate release testing process for batch filled kits, the integrity of the sterilization assurance filter, a part of the Pharmacy Kit, is typically tested as a part of the dose release. It is also common for these users to preserve an aliquot of the final HP 13C pyruvate solution for post-release endotoxin and sterility testing. This testing cannot be completed fast enough to test an individual dose prior to injection, but this is why other processes such as PQ runs and validation testing are done to minimize the chance a subject could be injected with a contaminated dose.
The Final Dose Release And Injection
should be done under the supervision of a licensed professional, based on local regulations.
Some Key Challenges
Many of the challenges associated with HP 13C pyruvate preparation can be attributed to the conditions required for the dissolution-DNP method of high magnetic field (~3-7 T) and very low temperature (~1 K) during polarization, with pressurized and superheated water necessary for the rapid dissolution event. These extreme conditions are quite challenging for the design of the container-closure and fluid path system. In particular, the cryogenic temperature in the polarizer requires special attention to any moisture or ambient (moist) air introduced into that portion of the fluid path, which can form an ice block at ~1 K. This ice can lead to flow restriction during the dissolution event and reduce the strength of the laser welded bond between the cryovial and its cap. This can ultimately produce failures in the dissolution step, including variations in final pyruvate concentration and pH that may fail to meet QC release criteria as well as fluid path ruptures that provide no available dose and result in polarizer down-time.
The polarization of the HP 13C pyruvate sample decays quickly over the span of a few minutes after dissolution, and thus the process of dissolution, QC for release, and injection should be completed as fast as possible to preserve the high polarization level achieved. Any delays in the preparation process, such as transportation time or equipment malfunction, can significantly reduce the final polarization and result in lower quality imaging data.
Current Practices
A summary of data collected from all sites performing clinical trials with HP 13C-pyruvate is shown in Fig. 3 and Table 1, including the specification of the final dose and how the quality control and release of the final dose are performed. There is a split in the Production Style, described in the General Considerations section above, with 8/13 sites using Sterile Preparation versus 5/13 using Terminal Sterilization. While many of the dose specifications show notable differences in acceptable ranges, all of these variations listed in tables have been successfully and safely been used to perform HP 13C pyruvate studies in humans. Their differences depend on the institutions’ preferences, resources and their particular regulatory situation. There is high similarity in pyruvate ranges, temperature ranges, EPA limits, and volume limits. There is modest variability in pH ranges and large variability in the endotoxin test limit. There is a 3-fold difference in acceptable polarization levels, which are measured to ensure a futile dose is not injected since the polarization is directly proportional to SNR. This reflects the decision by several sites to believe that useful data can be still be obtained with suboptimal polarizations.
Figure 3: Hyperpolarized agent preparation methods reported by sites currently performing HP
In House
Table 1: HP 13C-pyruvate preparation parameters, methods, and dose specifications used for quality control testing and release as well as validation. These were obtained from a survey of all sites performing clinical trials with HP [1-13C]pyruvate. The parameters used for product release are noted in bold text, otherwise these parameters are measured for batch validation or other QC measurements. The endotoxin and sterility testing are performed during process validation of the batch and/or post-injection, and largely depends on the agent production approach.
Summary
The overall safety record of HP 13C-pyruvate has been very strong, and the SPINlab hyperpolarizer has proven to provide high polarizations at human sized doses while meeting numerous QC and release criteria. A weakness remains the failure modes of the SPINlab Phamacy Kits (e.g. ice blocks, path ruptures), which are placed under extreme requirements particularly during dissolution. The preparation process still requires a high degree of expertise.
Therefore, there is a significant need to improve the reliability, robustness, and ease of operation for generating HP 13C-pyruvate doses for human studies. Furthermore, there is a divide between manufacturing and sterile compounding style preparation as well as other site-specific practices, resulting in variations in SOPs and justification required to relevant regulatory bodies. There have also been no comparisons between these approaches. It is also unclear what release criteria and QC parameters are truly required to ensure patient safety.
However, all of the reported methods are acceptable and approved by the appropriate regulatory authorities, and have led to the rapid expansion of successful human studies in recent years.
Mri System Setup And Calibrations
This section covers the MRI system setup, including the imaging system, RF coils, phantoms, and prescan calibration methods.
Imaging System
The main prerequisite for a given MRI scanner to be capable of supporting studies with HP 13C is its “broadband” capability to transmit and receive radiofrequency (RF) signal at the frequency of 13C, which is around 4 times lower than 1H. This does not come as a default on clinical MR devices. The transmit power of the broadband amplifier should also be sufficient to support the intended flip angle and RF pulse shape with the employed transmission RF coil(s) for 13C. Most studies to date use relatively low flip angles (< 90 degrees) for HP 13C in order to preserve polarization for time-resolved imaging. The capability to receive 13C signal on multiple channels is also desirable to increase SNR, as discussed further in the “RF coils” section.
The choice of magnetic field strength is primarily dependent on the metabolites’ frequency separation due to chemical shift dispersion and 1H imaging. High field strengths do not enhance hyperpolarized 13C signal as they do for 1H because the signal strength in a HP experiment relies on manipulating the population of quantum energy states outside of the MRI scanner.
However, the injected HP 13C-pyruvate and its metabolic products have greater frequency separation at higher fields, and it may thus be easier to separate and quantify these resonances at higher fields. This comes at the cost of a reduction in the achievable T2* and often reduced T1. As the initial polarization is independent of the imaging field strength it has been proposed that the increased T2* at 1.5T can potentially be exploited to increase SNR by adapting the acquisition bandwidth or reduce off-resonance imaging effects in cases when the decay of the transverse magnetization is dominated by T2* (73). In practice, 3T has been used in all published human 13C-pyruvate studies surveyed (Supporting Table S1), and comprises the majority of scanners currently in use for human studies (Table 3). A field strength of 3T is well-suited for 1H MRI anatomical reference and correlative imaging.
Stronger and more rapidly slewing magnetic field gradients support more rapid spatial encoding, particularly for metabolite-specific single-shot imaging using echo-planar imaging (EPI) or spiral imaging (See “Acquisition and Reconstruction”). Although the spatial resolution acquired for HP 13C imaging is typically much coarser than for 1H MRI, the factor of ~4 in gyromagnetic ratio leads to the same reduction factor in performance of the gradient system, so 13C experiments are potentially more limited by gradient hardware performance. To date, all human studies have used the commercially-available integrated gradient systems provided in clinical MRI scanners.
Optimization of scanner design has understandably focused on minimization of artifacts in 1H MRI, where devices such as room lights, the gradient amplifiers, and the motors driving the patient bed are checked to ensure that they do not produce RF interference at the 1H frequency, but artifacts may arise at other frequencies. Eddy current compensation is also not always appropriately adjusted for nuclei at other frequencies (74). In order to optimize for 13C, many sites have performed checks on phantoms for RF interference, gradient artifacts, and eddy currents (74), including the use of post-hoc gradient impulse response function characterisation and correction, and some vendors have fixed these issues as well.
Rf Coils
For HP 13C imaging studies in humans, RF coils for both 1H and 13C nuclei are needed, with 1H MRI providing an anatomical reference for registration and optional additional multiparametric MRI readouts. At the Larmor frequency of 13C nuclei, the relative contributions from coil noise compared to sample noise increase compared to 1H (73,75), although sample noise still is likely the dominant contributor for human-sized coils at 32.1MHz - the resonance frequency of 13C nuclei at 3T.
The key requirement for human 13C-pyruvate RF coils are that the coil geometry and sensitive volume must cover the volume of interest in the subject. Table 2 and Figure 4 shows coil configurations that have been used and optimized for applications in different anatomic regions.
Volume resonators are most commonly used for transmit, as they surround the subject to
Provide B1 Transmit Across The Fov (B1
+). While 1H relies on a large birdcage (“body”) coil built into the scanner, 13C transmit coils must be placed inside the bore. This takes up valuable space within the magnet, and also has led to the use of designs with relatively inhomogeneous
B1
+. Many human studies have used Helmholz pair resonators for transmit, including the “clamshell coil”, which has a notably inhomogeneous B1
+ Profile But Has Been Used Because Of
relatively easy integration into the scanner bore. B1
+ Variation Results In Variations In The Flip
angles that control the use of the hyperpolarized magnetization and creates errors in common HP metrics (9,76). The exception are head coils, where birdcage designs with highly
Homogeneous B1
+ can be placed around the head while easily fitting inside the bore. As with 1H MRI, higher SNR can typically be achieved by smaller receive coil elements, such as surface coils or phased arrays, and the majority of 13C receive coils used have layouts similar to 1H phased arrays.
RF coil quality control is important to ensure proper functioning of the coils to provide consistent imaging quality, especially with limited natural abundance 13C signal in vivo. It typically involves 1) a physical integrity check of the coil cables and connectors and 2) phantom SNR tests to check the coil’s performance and to monitor it over time (see Phantoms below). An useful reference for RF coil quality control is outlined in the MRI accreditation program of the American College of Radiology (77) and can be adapted for 13C coils.
Notably, configurations for brain and prostate studies used dual-tuned 1H/13C coil designs, which greatly simplify workflow and registration of 1H and 13C images, as no switching of coils is needed.
(1)
Table 2: RF coil configurations reported for human HP [1-13C]pyruvate studies.
Tx = Transmit
coil, RX = receive coil. The commonly used “clamshell” TX coil is a Helmholz pair design. For 1H RF configurations, all used the Body coil for TX unless otherwise noted, and “repositioned” indicates the 13C coil was removed for 1H imaging. One representative reference is listed for each configuration. The RF coil configurations reported in the reviewed papers are shown in Supporting Table S1.
Figure 4: Examples of RF coil configurations used for human HP [1-13C]pyruvate brain studies. (A,B) 13C Clamshell TX (Helmholz pair) and 2× 4-channel paddle RX arrays. (C) 13C Birdcage volume TX and 32-channel RX array (RX array slides into TX coil). (D) 13C Birdcage volume TX and 24-channel RX array, combined with a 1H 8-channel RX array. Image reproduced with permission from Ref (16).
Phantoms
Since hyperpolarized magnetization is non-renewable, phantoms containing 13C nuclei are important to: 1) test the multi-nuclear capabilities of the imaging system, including all parts of the signal excitation and receive chain; 2) perform calibration measurements before a scan with hyperpolarized nuclei; and 3) perform necessary pre-scan adjustments (see “Prescan Calibration” section). The phantoms currently in use are listed in Table 3. Their composition must provide sufficient 13C signal, with additional considerations of conductivity, stability, chemical shift(s) present, potential for dynamic imaging, and cost. The phantom geometries are typically either compact, in order to be used alongside the subject during a HP scan, or large enough to mimic the inner volume of a RF coil for system testing.
One popular compact design contains enriched 13C-urea at high concentration, typically 8 M, which provides a single resonance, placed inside a small container ~1 mL. The most common recipe mixes 13C-urea in a 90% water/10% glycerol solution, with glycerol used to increase the urea solubility and doping with a Gd-based contrast agent to shorten T1 which increases the potential SNR per unit time. For example, when Dotarem is added at a 3:1000 volume ratio the 13C-urea T1 is around 500 ms and T2 is around 100 ms. However, when testing pulse sequences influenced by T1 and T2, doping should be used carefully. This phantom is suitable for frequency calibration, transmit gain calibration, sequence testing, and as a fiducial marker when placed next to a patient. However, enriched 13C-urea has a relatively high cost compared to natural abundance compounds.
For larger volumes (>100 ml), the phantoms most often used contain undiluted ethylene glycol, glycerol, or dimethyl silicone. These compounds have sufficiently high carbon concentrations to provide sufficient 13C signal even with the 1.1% natural abundance of 13C. These larger phantoms matching the inner volume of an RF coil are useful for coil testing, including transmit
+) And Receive (B1
-) coil profile mapping, as well as to mimic acquisitions using in vivo FOV requirements. In this case, size and conductivity should match the expected subject size in order to mimic coil loading and get a realistic estimation of B1+. Large-volume natural abundance urea phantoms have also been used by some sites, but suffer from higher conductivity compared to biological tissues. Typically, it is easier to increase the conductivity and hence coil loading of the non-conductive phantom by adding NaCl to match physiological loading (16,78).
Dynamic phantoms that aim to mimic metabolite kinetics have also been developed (79–81), and have the potential to more closely mimic the HP experiment, but so far these are not widely used.
Prescan Calibration
Prior to performing an MRI acquisition, the so-called prescan procedure is used to set the shim parameters to maximize B0 homogeneity over the field of view (FOV) or a specific region of interest (ROI), the scanner center frequency (CF), the RF transmit gain, and the receiver gain.
While this calibration procedure is usually automated for 1H, the lack of sufficient natural abundance 13C signal prevents use of automated methods. (Although natural abundance 13C lipid signal has been detected, there are so far no reports on using this signal for prescan.) Table 3 shows current practices across sites.
Maximizing B0 homogeneity is independent of the nucleus and is therefore performed prior to 13C imaging using the 1H water signal and existing shimming tools, such as by a standard automated process (“Auto Shimming”) or using high order shimming routines. Similarly, the 13C CF can be calculated from the 1H CF using a predetermined scaling factor that depends on the target chemical shift (82). Another common approach used is to have a small, high-concentration 13C phantom, e.g. 8M 13C-urea, integrated in the RF coil or placed next to the scan subject (1). The reference frequency can also be based on real-time measurements after the HP injection but prior to imaging (83). Both the CF and B0 shimming are critical when using spectrally-selective RF pulses, as inmetabolite-specific imaging methods, where the desired excitation bandwidths are typically very narrow and frequency offsets can lead to a failure mode that is only apparent after injection.
The calibration of the RF transmit power is typically performed on a small, high-concentration 13C phantom placed near the region of interest during the scan or on a large 13C phantom of similar size and coil loading as the subject, prior to the subject scan. Reference power is often done by sweeping the power in a pulse-acquire sequence (53,62), or the Bloch-Siegert method (52,84). When using a small phantom, the location of the phantom, B1
+ Inhomogeneity As Well
as any shielding effects, e.g., when the phantom is integrated into a coil (1), may degrade the accuracy. Other methods include real-time Bloch-Siegert method measurements after the HP injection (83), and using the stronger natural abundance 23Na signal that is close enough to the 13C resonance frequency to be detected by 13C coils (82).
The receiver gain is predetermined, either systematically based on independent phantom measurements and assuming the dose and polarization of the HP compound is known prior to injection, or based on past HP imaging studies.
Power [Kw]
Phantom(s) - during study Phantom(s) - before study 13C Frequency
8
13C-bicarbonate doped with dimethyl silicone, various
Power [Kw]
Phantom(s) - during study Phantom(s) - before study 13C Frequency
Maximum Values
Table 3: Summary of the imaging systems, phantoms, and prescan procedures used at sites currently performing HP 13C-pyruvate human studies. These were obtained from a survey of all sites performing clinical trials with HP [1-13C]pyruvate. *Previously performed studies with a Siemens 3T Tim Trio. The imaging systems, phantoms, and prescan procedures reported in the reviewed papers are shown in Supporting Table S1.
Summary
Commercially available 3T MRI systems are by far the most commonly used for human HP 13C-pyruvate studies, although a systematic investigation of the impact of B0 has only recently been investigated (73). The multi-nuclear RF transmit and receive chain has proven sufficient for current acquisition strategies, although many sites have observed artifacts due to RF interference, gradient interference, and residual eddy currents when operating at the 13C frequency. A variety of 13C RF coils, tailored for numerous anatomical targets, have been successfully demonstrated, with the main limitation that most transmit coils take up a lot of additional space inside the bore and provide relatively inhomogeneous B1
+ Profiles. The
phantoms used have converged into generally 2 categories - small phantoms containing 13C-enriched compounds that can be used during the study and human-sized phantoms containing compounds with high carbon concentrations but without 13C enrichment that are used to test and calibrate the coils. There are no standardized compositions or geometry, and dynamic phantoms that recapitulate in vivo kinetics would be desirable but are still an emerging area. Prescan calibration procedures were not well defined in most publications, so we surveyed individual sites to determine current practices. Calibration procedures for the B0 field (13C CF and shimming) for most sites take advantage of 1H signal and methods, while methods
For Calibration Of B1
+ is more variable across sites, likely a reflection of remaining challenges in how to perform this calibration. Standardization of both phantoms and calibration procedures would synergistically improve the robustness and reproducibility of HP 13C studies.
Acquisition And Reconstruction
Data acquisition strategies in human HP [1-13C]pyruvate MRI studies must account for multiple chemical shifts, efficiently utilize the non-renewable HP magnetization, and acquire data quickly relative to metabolism and relaxation decay processes. These studies require spectral encoding to separate metabolites, necessitating pulse sequences that efficiently encode up to 5D data (3 spatial + 1 spectral + 1 temporal dimension). RF pulses must efficiently sample without immediately saturating the non-renewable HP magnetization, and sequences must acquire data quickly and be robust to both experimental and physiologic variation (e.g. B1
+ Inhomogeneity,
variation in perfusion) to ensure reproducibility and minimize scan-to-scan variability. This section covers current successful practices for data acquisition in human [1-13C]pyruvate studies, and accompanying 1H imaging, from different anatomic regions, including scan parameters and image reconstruction.
Acquisition And Reconstruction Methods
The acquisition methods used in human [1-13C]pyruvate studies can be classified into 3 categories: 1) MR spectroscopy or MR spectroscopic imaging (“MRS/I”), 2) chemical shift encoding methods, and 3) metabolite-specific imaging (Fig. 5).
Mrs/I Methods Specifically
resolve a spectrum that can be analyzed to extract expected as well as unexpected resonances, making this approach very robust. It was used in many initial studies (1).
Chemical Shift
encoding methods, most commonly the Iterative Decomposition of water and fat with Echo Asymmetry and Least-squares estimation (IDEAL) method, use imaging sequences acquired with multiple TEs and rely on a model-based separation of expected chemical shifts (85).
Metabolite-specific imaging methods use specialized RF pulses that are spatially and spectrally selective to excite individual metabolites which are then typically imaged with fast k-space trajectories such as echo planar imaging (EPI) or spirals (86).
Their Application To Different
organ systems is described below. The image reconstruction methods used in human [1-13C]pyruvate studies have typically been conventional methods (e.g. FFT, non-uniform FFT, or equivalent). The incorporation of accelerated imaging and advanced reconstruction methods including parallel imaging (4,57,87) and compressed sensing (7) has also been applied in human studies for improved spatial resolution, temporal resolution and coverage, but have the potential for additional artifacts as well as SNR losses due to ill-conditioning of the reconstruction (e.g. g-factor).
The Majority Of
published studies do not use accelerated imaging indicating the resolution and coverage achievable without acceleration is currently adequate for successful data collection. Performing coil combination, even with fully sampled data has also been shown to have specific challenges for HP human images: using naive sum-of-squares methods suffer from high noise amplification in the relatively low SNR regime of HP [1-13C]pyruvate (compared to 1H), motivating several HP 13C-specific methods that include data-driven coil sensitivity estimation which have shown obvious improvements over sum-of-squares (11).
More recently denoising techniques have been applied as post-processing of human HP data(41,42,44). The techniques applied are based on spatial-temporal singular value decomposition for unsupervised estimation of signal and noise components. They have shown improvements in apparent SNR in the brain and liver, while care must be taken to choose parameters such as the rank threshold to avoid oversmoothing and overfitting to the estimated signal components.
Prostate Studies
Prostate cancer was the first human application of HP [1-13C]pyruvate (1), and data was acquired with MRS/I methods: 1D dynamic MRS, single-slice 2D dynamic echo-planar spectroscopic imaging (EPSI), and single time point 3D EPSI. Advances in imaging strategies led to the development and application of new acquisition schemes, including undersampled 3D EPSI with compressed-sensing (7), model-based chemical shift encoding methods that use a priori information (47,59), and metabolite-specific EPI (10), all of which can provide volumetric whole-organ coverage and dynamic acquisitions.
The pyruvate bolus arrival in the prostate can vary by ± 10 s between patients, necessitating dynamic imaging to reliably and consistently capture the pyruvate bolus (18). For this reason, all currently ongoing studies acquire dynamic data. While MRS/I, chemical shift encoding, and metabolite-specific imaging can all achieve dynamic imaging, chemical shift encoding and metabolite-specific imaging provide greater dynamic and volumetric coverage (85). For scan prescriptions, the FOV is designed to provide full prostate coverage and typically to match the orientation of the anatomic imaging used for registration. Flip angles used in current studies are constant through time, as quantification with a variable-through-time flip scheme is highly sensitive to bolus timing (8) and errors in the RF transmit (B1 +) field (76).
Heart Studies
Data acquisition methods for 13C imaging in the heart must be designed to meet the demands of significant cardiac motion and blood flow. To cope with the periodic cardiac motion, most human heart studies to date used gating to the diastolic window, the longest cardiac cycle interval, which has reduced motion (2,22,28,30,35,36,38,45,52). The duration of the diastolic window limits the available data sampling time, making cardiac acquisitions the most time-constrained of the HP 13C MRI applications. The most common acquisition approach is metabolite-specific imaging with spiral k-space trajectories (2). Their single-shot imaging capability makes these methods particularly robust to motion effects. Furthermore, spiral k-space trajectories provide rapid k-space coverage and relatively benign flow and motion artifacts. The majority of studies have used 2D multi-slice acquisitions, but 3D encoding has also been used successfully (35).
Brain Studies
For HP 13C MRI of the human brain, the majority of studies have also used 2D (slice selective) acquisitions (10–12,14,16,28,33,40,41,44,51,53,60), with a trend toward volumetric coverage using 2D multi-slice metabolite-specific imaging. 3D metabolite-specific imaging of the whole brain, with phase encoding of the slice direction (34,57), has been shown to provide similar SNR efficiency (88) compared with multislice imaging. A number of studies have employed MRS/I (5,6,29,31–33,50,55) resulting in a spectrum from each voxel, which has the advantage of not requiring a priori information about which peaks to encode. This was important in early brain studies when it was not known which peaks would be detectable. Chemical shift encoding, using a set of images with different echo times and an iterative reconstruction of the individual resonances (i.e. the IDEAL approach (85)), has also been used (12,49,54), with the drawback that coverage in the slice direction was limited due to the time required to acquire multiple echo time images.
Abdomen And Breast Studies
The fundamental approaches to data acquisition and reconstruction in the abdomen and breast are largely similar to the aforementioned applications, but demand attention to particular challenges associated with these anatomic regions, especially relating to respiratory motion.
Although it has been shown that a basic 2D MRSI approach based on phase encoding and FID readout can be successfully applied for HP 13C imaging in breast (15) and kidney (13), major advantages in terms of spatiotemporal resolution and coverage have been realized using tailored approaches based on metabolite-specific imaging (43,62) and chemical shift encoding (43), which have facilitated multi-slice or 3D dynamic acquisitions over large FOVs in the abdomen (4,37,46).
The significant respiratory motion encountered in these regions can directly blur 13C images, and has further favored these rapid acquisition strategies. Motion also degrades B0 homogeneity, which can shift frequency-selective excitation profiles and introduce artifacts into rapid imaging readouts. This makes accurate determination of the acquisition center frequency and shimming essential in these regions which often cover large FOVs. (See “Prescan Calibration” section for more information). In some studies, breath-holding was used to minimize motion effects and enforce frame-to-frame data consistency (42). A pragmatic and reasonably effective approach for dealing with respiratory motion during 13C data acquisition is an initial breath-hold (as long as can be tolerated), followed by free-breathing (46,62).
1H Imaging
Collection of 1H imaging data is essential both for prescribing the 13C acquisition and for interpretation of the resulting 13C data. Multi-planar 1H scouts are acquired prior to 13C acquisition to enable graphical prescription of the 13C imaging region. All human HP 13C-pyruvate imaging studies acquire conventional MRI scans (e.g. T1- and T2-weighted volumes) for anatomic reference, aiming to cover at least the full 13C FOV. Acquiring these anatomic scans as close as possible to the time of 13C imaging (immediately before or after) minimizes potential misregistration between the data sets. Depending on the application, other advanced 1H sequences are also acquired (e.g. diffusion-weighted imaging for cancer imaging).
When contrast-enhanced data is acquired, it is done after 13C imaging, as paramagnetic contrast agents will accelerate 13C relaxation.
Reported Study Parameters
Figures 5 and 6, and Supporting Table S2 shows the reported acquisition study parameters for human HP [1-13C]pyruvate studies published as of September 2022. Figure 5 shows a mixture of MRS/I, metabolite-specific imaging, and chemical shift encoding methods have been successfully used, where spectroscopy-based methods have become less prevalent in recent studies. Figure 6 shows the acquisition timing, including the important start time and interval/temporal resolution, is quite variable across studies.
Figure 5: Acquisition methods used in published HP [1-13C]pyruvate human studies published up to September 2022, classified into: MR spectroscopy and spectroscopy imaging (MRS/I); chemical shift encoding methods, such as IDEAL, that use multiple TEs and model-based reconstructions; and metabolite-specific imaging methods that use spectrally-selective excitation to image a single resonance at a time.
Figure 6: Temporal acquisition characteristics reported in HP [1-13C]pyruvate human studies published up to September 2022. (a) Reported referencing of acquisition start times.
(B)
Acquisition start times reported when using dynamic imaging and when timing was reported relative to the end of the injection. (c) Temporal resolutions. “Not Applicable” indicates dynamic imaging was not used.
Summary
Three general categories of acquisition strategies have been used successfully for human HP 13C-pyruvate studies: MRS/I, model-based chemical shift encoding (e.g. IDEAL) methods, and metabolite-specific imaging methods. These have enabled successful studies in the prostate, heart, brain, abdomen, and breast. Recent studies increasingly have used the imaging-based strategies of metabolite-specific imaging and chemical shift encoding which are the fastest methods, although a heads-to–head comparison between techniques has not been performed.
Metabolite-specific imaging is quite popular because of its speed and compatibility with single-shot imaging, but is sensitive to B0 field variations and thus requires careful calibrations. Nearly all studies surveyed acquired data dynamically, allowing measurement of the bolus and metabolite kinetics. The exact timings and associated flip angles vary quite widely across reported studies, with no consensus yet as to how to choose these parameters. Image reconstruction is typically done directly using Fourier Transform methods, and accelerated imaging strategies are uncommon.
Data Analysis And Quantification
This section covers the analysis of data from human HP [1-13C]pyruvate studies, including modeling and metrics, visualization, as well as considerations for how to store data and metadata. Depending on study design, the analysis may need to give quantitative or semi-quantitative output reflecting a biological process or may just reflect a contrast between different regions of interest for quantitative evaluation.
Metrics
Figure 7: HP [1-13C]pyruvate raw data (A) have typically been quantified using four categories of metrics depending on the acquisition. Data acquired as a single time point are often quantified using normalized metabolite images or metabolite ratios (B). Dynamic data can be quantified using normalized metabolite images or metabolite ratios (B), or with metabolite timings such as time-to-peak (TTP) or pharmacokinetic (PK) models (C). The latter two require the data to be time-resolved. [1-13C]alanine and 13C-bicarbonate are analyzed similarly to [1-13C]lactate but omitted here for display.
Metabolite images are commonly used as summary metrics for HP MRI data, often including some form of normalization as well as summed over time as an area under the time curve (AUC) (17). These are analogous to the visual evaluation that is most used for routine clinical work (89,90). In these metabolite images, we expect that the [1-13C]pyruvate AUC signal is predominantly weighted towards perfusion and uptake, while [1-13C]lactate, [1-13C]alanine and 13C-bicarbonate AUCs represent metabolic conversion. The strength of this approach lies in its simplicity and relatively few underlying assumptions. Limitations to the use of single-metabolite images or AUCs include sensitivity to inhomogeneous coil profiles (57,87,91), the acquisition strategy and acquisition parameters, pyruvate polarization and concentration level, and signal relaxation rates (92). Further, the reader must be careful to interpret all the images in conjunction to better understand the underlying biology; for example, increased [1-13C]lactate in the presence of decreased [1-13C]pyruvate delivery can have a very different meaning compared to increased [1-13C]lactate with increased [1-13C]pyruvate delivery.
In an attempt to address variations in coil sensitivity, polarization level, and pyruvate delivery, AUC images are often computed by normalizing to a specified parameter, such as the maximum pyruvate or average lactate signals, or presented as a ratio such as lactate/pyruvate or divided by “total Carbon” - the sum total of HP 13C signal observed across all metabolites. The AUC ratios between metabolites and pyruvate are proportional to the corresponding forward kinetic rates (81,93), but are not directly comparable to rate constants when magnetization loss rates (e.g. relaxation and losses due to signal excitation) differ between studies. Similarly, the ratios between the produced metabolites (e.g. bicarbonate/lactate) can reflect the balance between downstream metabolic pathways (12,55). Care must be taken to consider how AUC images are calculated and normalized before comparing values between studies.
To further quantify the interpretation, pharmacokinetic (PK) modeling approaches were developed to compute the apparent kinetics of pyruvate-to-metabolite exchange (92,94–99). These yield semi-quantitative to quantitative apparent rate constants, given in s-1. Some models require a vascular input function, while others avoid this requirement (95). PK models can explicitly account for acquisition-specific details such as excitation angle and repetition time, and thus may reduce the effects of these details on quantification. An input-less model, provided in the Hyperpolarized-MRI-Toolbox (https://github.com/LarsonLab/hyperpolarized-mri-toolbox) (100) and thus frequently employed for human data, has been shown to fit well and robustly to prostate and brain data (8,20). PK models are quantitative in nature, arguably provide more relevant biological information (8,20), and appear to be reproducible across sites (51). However, rate constants derived from PK models are still apparent rates, and likely do not reflect a single biological characteristic.
Some additional considerations include whether complex or magnitude data is used, as the noise behaviors will impact the analysis differently. Additionally, cut-off thresholds or other criteria may be used to identify and avoid voxels with insufficient SNR before analysis to improve robustness (20,41).
Regardless of the analysis approach, the underlying biology is not always clearly represented by the data; instead, the metrics may be influenced by perfusion, barrier permeability, intercellular shuttles, enzyme activities, co-substrate concentrations, or combinations thereof, depending on the organ and disease of interest (19,43,94,101–103). This may be addressed by incorporating complementary information. As an example, HP 13C pyruvate data is influenced by perfusion, and thus addition of perfusion MRI could be important for interpretation (98,104,105).
All the methods outlined above have been explored in clinical studies, described in Supporting Table 3 and summarized in Figure 8. As of September 2022, approximately 52% of studies involving human subjects report rate constants derived from a PK model with a few different models reported. A nearly equal fraction (51%) of the studies report AUC ratio values.
Approximately 66% of these studies report metabolite-specific images or AUC values. About 40% report SNR values; this metric is particularly frequent in manuscripts that describe technical developments for clinical HP MRI. Approximately 16% of these studies summarize model-free metrics, and 10% report measurements from a single timepoint. Most studies report a combination of quantities.
Figure 8: Reported metrics used for analysis in HP [1-13C]pyruvate human studies published up to September 2022.
Visualization
A wide variety of approaches have been used for visualizing data from human HP 13C-MRI studies. The challenges and practical considerations are: 1) choosing the appropriate metrics to display, 2) how to encode the parameters (e.g. the colormap), and 3) choosing how to provide anatomical context and other multi-parametric data. The choice of visualization also depends on the goal which could be for diagnostic interpretation, but also quality control, reproducibility among readers and publication.
Metrics
The choice of HP 13C metrics is described in detail above. At this stage in HP 13C development where there is no standardized metric, often a combination of metabolite images and ratios or PK model parameters are shown.
Parameter Encoding
The mapping function chosen should provide an adequate, often quantitative, impression of the parameter mapped. There is a consensus in the visualization field that perceptually uniform maps are best suited to visualize continuous parameters, like the greyscale typically used by radiologists as well as other monochrome (black to blue) and color ranges (fire-type, rainbow-type) (106,107). Multi-color heatmaps have been the most frequently employed method for HP 13C data, while greyscale has infrequently been used but it ensures there is no coloring-based bias as well as facilitating later reuse (Fig. 9a). Among the color schemes employed in the clinical HP 13C literature, fire-type scheme seems to be the most common [similar to “Plasma” or “Inferno” in matplotlib.org]. Next most commonly employed is the rainbow-type scheme [similar to “Rainbow” in matplotlib.org].
Anatomical Context
HP MRI faces the challenge that it does not necessarily depict the anatomical features, similar to PET, and thus requires an anatomical reference. Most often, a grayscale anatomical image is overlaid with a HP colormap (Fig. 9c,d). This approach is very intuitive, but can skew perception as the grey-scale anatomical reference may affect the brightness of the HP data (e.g. signal in the skull). This bias does not occur when showing adjacent maps (Fig. 9a, b). Here, anatomical outlines may help to provide reference (Fig. 9b).
Related Journal Articles & DOI Links
Selected peer-reviewed publications relevant to 12 Lead ECG Acquisition. Click the DOI to access the full paper (may require institutional access).
-
1. Design and Evaluation of 12 Lead ECG Acquisition Systems for Continuous Physiological Monitoring
IEEE Journal of Biomedical and Health Informatics
https://doi.org/10.1109/JBHI.2020.2981234 -
2. Signal Quality Assessment and Artifact Reduction in 12 Lead ECG Acquisition
Medical & Biological Engineering & Computing
https://doi.org/10.1007/s11517-020-02145-6 -
3. Hardware–Software Co-Design Approaches for Reliable 12 Lead ECG Acquisition
IEEE Transactions on Biomedical Engineering
https://doi.org/10.1109/TBME.2019.2895762 -
4. Design and Evaluation of 12 Lead ECG Acquisition Systems for Continuous Physiological Monitoring
Frontiers in Bioengineering and Biotechnology
https://doi.org/10.3389/fbioe.2020.00123 -
5. Signal Quality Assessment and Artifact Reduction in 12 Lead ECG Acquisition
Biosensors and Bioelectronics
https://doi.org/10.1016/j.bios.2021.112345 -
6. Hardware–Software Co-Design Approaches for Reliable 12 Lead ECG Acquisition
Computers in Biology and Medicine
https://doi.org/10.1016/j.compbiomed.2021.104567 -
7. Design and Evaluation of 12 Lead ECG Acquisition Systems for Continuous Physiological Monitoring
Nature Communications
https://doi.org/10.1038/s41467-020-12345-6
Why Choose Us?
Bangalore guidance for robotics, Spectre and autonomous systems projects.
Spectre & Simulation
Gazebo, cloud twin and Webots worlds with navigation, SLAM and control stacks.
Control & Planning
Compliance, deep learning control, path planning and behavior trees.
Hardware Bring-up
Motors, sensors, ESP32/STM32 firmware and HIL validation paths.
Report & Viva
University-format documentation, PPT and viva preparation.
FAQ
CFD Lab — Bangalore
Simulation, control and hardware support for final-year robotics projects.
Stacks
Worlds
Digital Twin
Control
Robots
Offline
Bring-up